Last updated: September 2026 Written by: Richard, Qingdao ACTA Biotechnology Co., Ltd. Technical review: Alice Meng Topic:MCC in Almond Milk
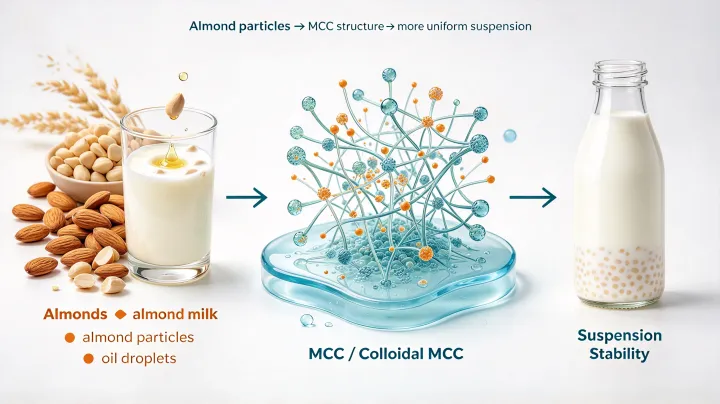
Caption:MCC can support suspension structure in almond milk when grade, dosage, dispersion, and processing are properly controlled.
Almond beverages can contain insoluble almond particles with different sizes and densities. Oil, proteins, mineral fortification, and heat treatment can further change how those particles and droplets behave during processing and storage. As a result, an almond milk formula that appears uniform immediately after production may develop sedimentation, creaming, serum separation, or poor redispersibility later in shelf life.
MCC in almond milk gives formulators a practical way to address part of this stability challenge. Microcrystalline cellulose (MCC), especially colloidal MCC or MCC-based beverage systems, can contribute to suspension structure and help keep insoluble particles more evenly distributed. Formulators may also combine MCC with CMC when additional control of the continuous phase or mouthfeel is needed.
This guide covers dosage, grade selection, MCC + CMC systems, processing, troubleshooting, and supplier selection, so your formulation and purchasing teams can evaluate MCC for almond milk in one place.
Adding MCC does not automatically guarantee a stable beverage. The result depends on MCC grade, dosage, particle size, dispersion, hydration, homogenization, almond solids, oil, protein, pH, and heat treatment. So the practical question is not “Can MCC stabilize almond milk?” A better question is:
“How should MCC be selected, dispersed, dosed, and combined with other stabilizers to achieve the required stability in almond milk?”
Quick answer: MCC in almond milk can support suspension structure and help reduce visible sedimentation when the grade, dosage, dispersion, hydration, and processing conditions are appropriate. Colloidal MCC is commonly evaluated for beverage suspension applications, while some formulations may benefit from an MCC + CMC system. There is no universal dosage, so screen candidate grades in your own formula and confirm performance through pilot, commercial, and shelf-life validation.
| Question | Practical answer |
|---|---|
| Main role of MCC | Suspension structure |
| Best form to evaluate | Colloidal MCC / MCC-based beverage system |
| Starting dosage | Screen a formulation-specific range |
| Key process variables | Dispersion, hydration, homogenization |
| MCC + CMC | Useful when additional water-phase control is needed |
| Validation path | Lab → pilot → commercial → shelf life |
This guide is intended for beverage R&D teams, food technologists, QA/QC professionals, purchasing teams, and manufacturers evaluating MCC or colloidal MCC for almond milk and other plant-based beverages. It is particularly useful when a formulation shows sedimentation, creaming, serum separation, poor redispersibility, or instability after homogenization or heat treatment.
| Step | Action |
|---|---|
| 1 | Define the instability (sedimentation, creaming, serum separation, or texture) |
| 2 | Check almond particle size and homogenization |
| 3 | Select a candidate colloidal MCC grade |
| 4 | Screen dosage under identical processing conditions |
| 5 | Optimize dispersion and hydration |
| 6 | Evaluate an MCC + CMC combination |
| 7 | Validate homogenization and thermal processing |
| 8 | Run shelf-life testing (Day 0–30+) |
| 9 | Test performance across multiple MCC lots |
| 10 | Confirm the supplier and lock the specification |
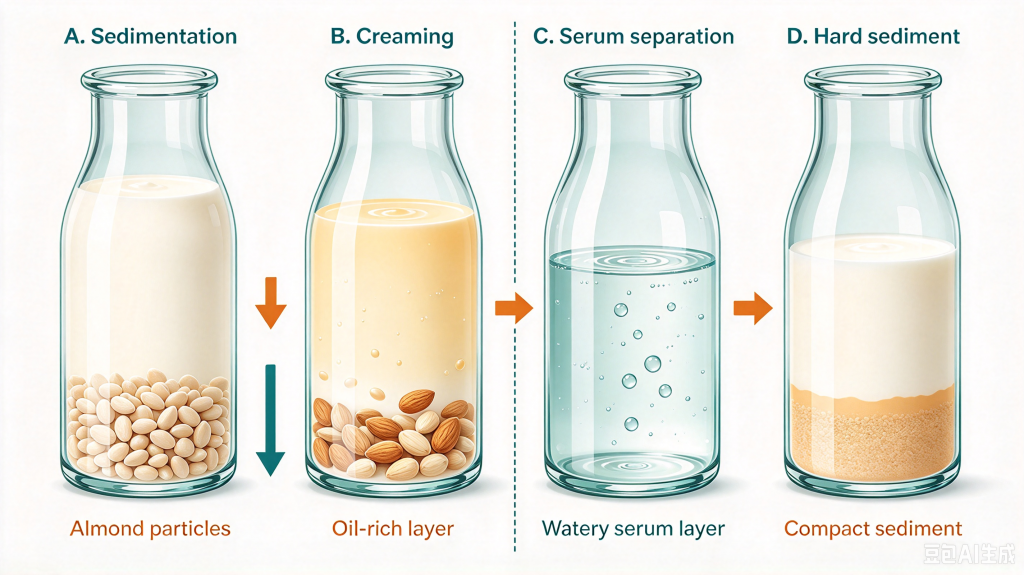
Caption:MCC can support suspension structure in almond milk when grade, dosage, dispersion, and processing are properly controlled.
Almond milk is a multi-phase beverage in which almond solids, water, oil, proteins, minerals, and other ingredients interact during processing and storage. Without an appropriate stabilization system, manufacturers may see:
A good almond milk stabilizer system balances two goals at once: physical stability and drinking quality.
In almond milk, MCC is primarily evaluated for its ability to contribute to suspension structure rather than simply increase bulk viscosity. When a suitable colloidal MCC system is properly dispersed and hydrated, it can help create a more structured continuous phase that slows the movement of insoluble particles.
The practical objective is therefore not to maximize viscosity. Instead, formulators need enough structure to improve particle suspension while preserving pourability, drinkability, and acceptable mouthfeel.
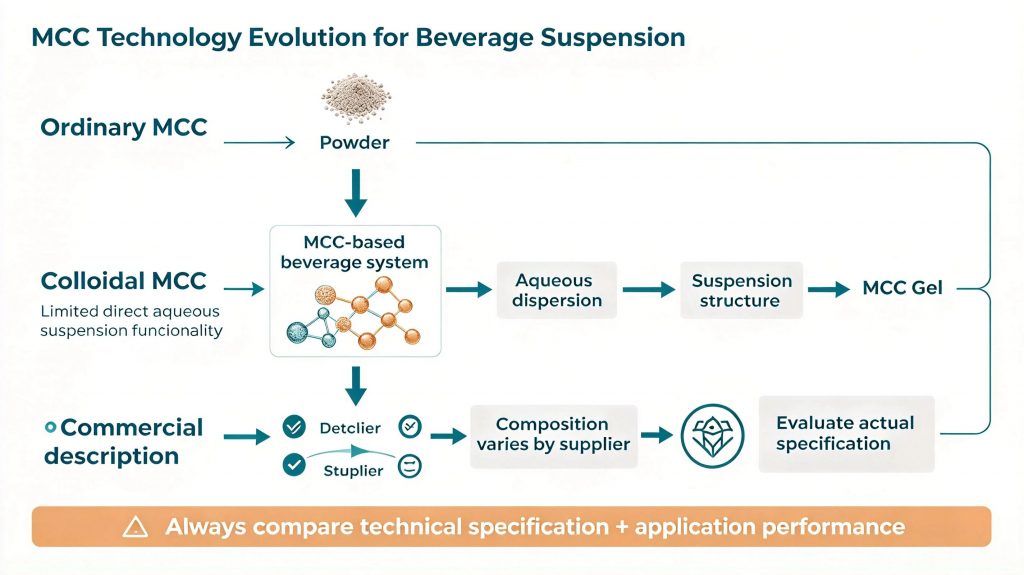
Not every MCC is interchangeable in beverages.
Ordinary MCC vs. colloidal MCC. Traditional MCC is a powdered cellulose material, while colloidal MCC refers to MCC-based systems designed or processed for aqueous dispersion and suspension applications. The exact composition, processing method, and functionality can vary by supplier. Therefore, a food-grade MCC specification alone does not establish that the material will provide the same functionality as a beverage-oriented colloidal MCC system.
What does “MCC gel” mean? “MCC gel” is commonly used as a commercial description for certain colloidal MCC-based systems rather than as a single universal technical specification. Composition, CMC content, activation requirements, viscosity, and suspension performance can vary between suppliers. Always evaluate the actual technical specification and application behavior rather than comparing products by the name “MCC gel” alone.
Regulatory status varies by market. MCC and sodium CMC are used as food additives in multiple regulatory frameworks, but permitted uses, specifications, and labeling requirements vary by market. Manufacturers should confirm the applicable requirements for the target market before commercial use.For the United States, manufacturers should verify the applicable requirements in the current FDA food regulations.For EU applications, manufacturers should check the current EU Food Additives Database and applicable conditions of use.
When evaluating a candidate MCC, ask: Is it designed for beverage use? Does it contain CMC, and at what level? What dispersion or hydration does it need? Does it remain stable after homogenization and heat treatment? Can the supplier provide application data and consistent supply?
Can MCC reduce almond milk sedimentation? It can help, and the physics explains why. Stokes’ law, a standard starting point for suspension stability, describes settling speed:
v = 2r²(ρp − ρf)g / 9μ
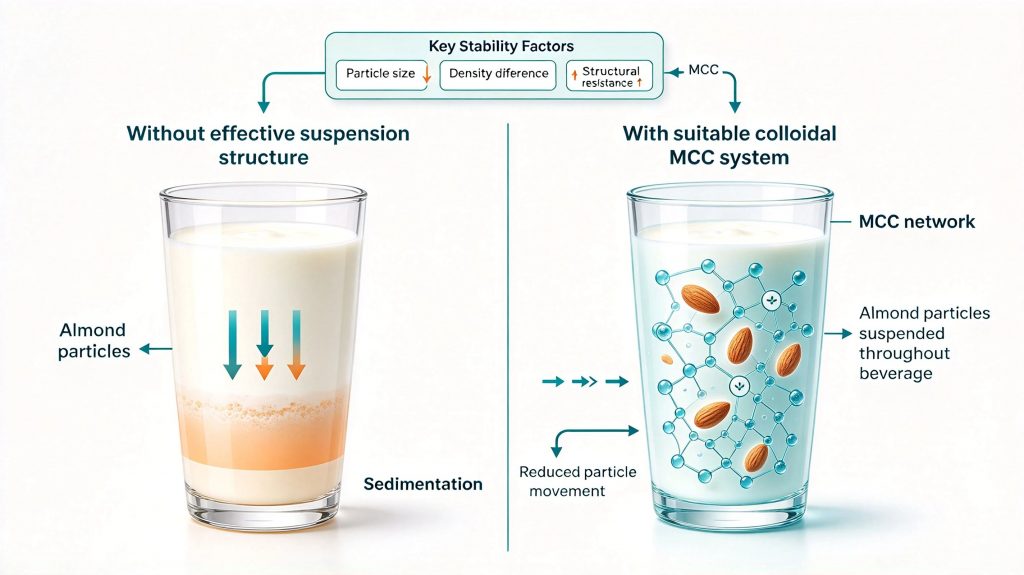
Settling speed rises with the square of particle radius and with the density difference between particle and liquid. In a simplified model, settling velocity decreases as the continuous phase offers greater resistance to particle movement. Homogenization can reduce effective particle or droplet size, while an MCC-based system can increase the structural resistance of the continuous phase.
Stokes’ law is a useful conceptual model, but real almond beverages are non-ideal systems. In practice, particles may aggregate, interact with proteins or minerals, or move through a structured rather than purely Newtonian continuous phase. For this reason, two almond beverages with similar measured viscosity can still show very different sedimentation behavior. The relevant question is not only how viscous the beverage is at one test condition, but how the stabilizer system behaves under the shear and storage conditions the product actually experiences
A useful formulation target is therefore a system that provides sufficient structure at rest while still allowing practical processing and acceptable drinking properties under shear.
Sometimes, but creaming differs from sedimentation — one is downward particle movement, the other is upward oil droplet movement. If a cream layer persists even though particles stay suspended, investigate oil droplet size, homogenization, and the emulsifier system before increasing MCC.
The suspension network. Under suitable dispersion, hydration, grade, and concentration conditions, some colloidal MCC systems can develop a structured aqueous phase with yield-like behavior that helps resist particle movement. Depending on grade, concentration, and beverage composition, these systems may also exhibit shear-thinning behavior, so the beverage can still pour and drink smoothly. Judge stability by sedimentation, creaming, redispersibility, and appearance over time — not by a viscometer reading alone.
The timing of a failure is often as informative as its appearance. Record whether instability appears before homogenization, immediately after heat treatment, after cooling, or only during storage, because the timing can help narrow down the likely cause.
| Symptom | Typical causes to check |
|---|---|
| Sediment at the bottom | Large almond particles, insufficient homogenization, poor MCC dispersion, unsuitable grade, insufficient hydration |
| Cream layer on top | Large oil droplets, weak emulsion structure, unsuitable emulsifier system |
| Serum separation | Weak network, incomplete hydration, mineral or protein interactions |
| Hard, compact sediment | Particle aggregation, poor dispersion, mineral/protein interactions, long storage |
| Too thick | Excess MCC, CMC, starch, or other hydrocolloids; high solids |
| Stable before heat, unstable after | Hydration, homogenization, thermal step, protein and mineral behavior |
Loose sediment vs. hard sediment. Loose sediment forms a soft layer that redisperses after gentle inversion. Hard sediment forms a compact layer that resists redispersion and needs closer investigation into particle size, dispersion, hydration, processing, and mineral or protein interactions.
What type of almond milk are you producing — standard, high-solids, fortified, barista, or shelf-stable? Barista formulations may require separate evaluation because steaming, heating, and coffee interaction can change the stability and sensory requirements.
Screen at least two candidate grades under identical conditions — same almond base, dosage, mixing, homogenization, and thermal treatment.
Supplier selection rule: Do not choose colloidal MCC by viscosity alone. Compare suspension performance, dispersion behavior, mouthfeel, processing tolerance, lot consistency, and cost-in-use under the same formulation conditions.
| Factor | What to compare |
|---|---|
| MCC type | Ordinary vs. colloidal; CMC included or not |
| Viscosity specification | Value and test method/concentration |
| Particle characteristics | Particle size or mesh specification |
| Moisture/LOD | COA values across batches |
| Application performance | Sedimentation, creaming, redispersibility, mouthfeel |
| Recommended dosage | Supplier’s screening range |
| Documentation | TDS, COA, SDS, food-grade documents |
| Supply | Capacity, lead time, MOQ, change control |
| Cost-in-use | Price × effective dosage |
The table below is a starting reference, not a ranking.
| Stabilizer | Main functional role | Typical reason to evaluate | Key consideration |
|---|---|---|---|
| Colloidal MCC | Suspension structure | Sedimentation control | Grade, dispersion, hydration |
| CMC | Water-phase rheology | Viscosity and serum control | Dosage and mouthfeel |
| Xanthan gum | Thickening / suspension support | Strong rheological effect | Can affect texture |
| Modified starch | Body and texture | Mouthfeel, processing tolerance | May not replace suspension structure |
| Gellan gum | Suspension / structuring | Fine particle suspension | Can create a more structured texture |
| Pectin | Stabilization / mouthfeel | Certain acidic or protein systems | Depends strongly on formulation |
The goal is not to identify a universally “best” stabilizer. The appropriate system depends on particle load, oil and protein content, target texture, processing conditions, and regulatory requirements.For a broader comparison of stabilizer systems used in plant-based beverages, see our guide to plant-based milk stabilizers, including MCC, CMC, and modified starch.For a broader overview of beverage stabilizer selection, see our food stabilizers for beverage systems guide.
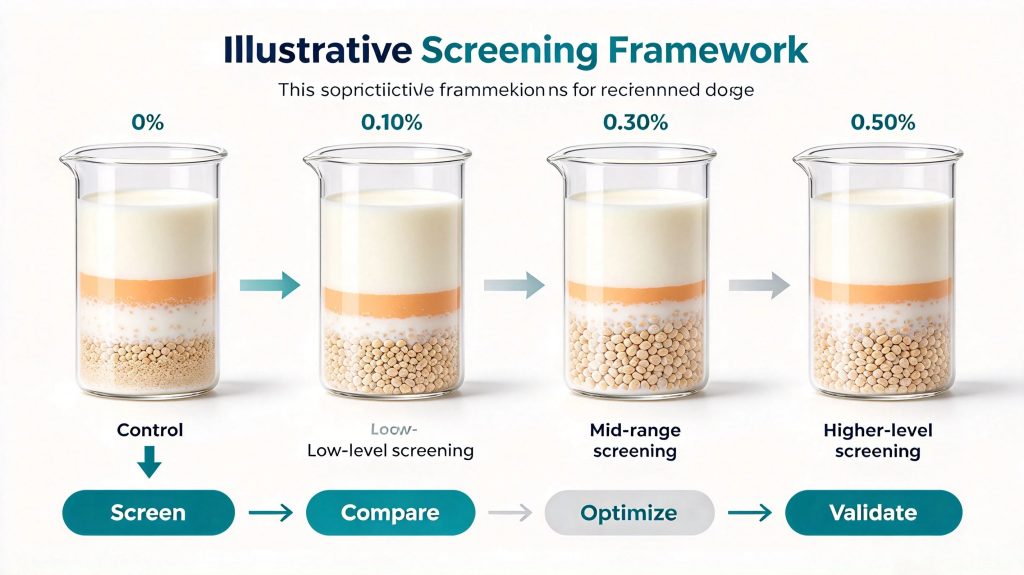
Dosage depends on almond solids, particle size, protein, calcium, sugar, homogenization, heat treatment, and target mouthfeel. Treat MCC dosage as something to screen and optimize — not something to copy from a table.
Important formulation note: The 0.10%–0.50% range in this guide is an illustrative screening example for initial laboratory work, not a universal dosage recommendation.
| Trial | MCC screening level | Main objective |
|---|---|---|
| Control | 0% | Baseline |
| A | 0.10% | Low-level response |
| B | 0.30% | Mid-range response |
| C | 0.50% | Higher-level response |
If performance improves strongly between 0.10% and 0.30%, the higher level may not add much benefit. If 0.50% produces little additional improvement, treat this as a possible sign of diminishing returns. Fine-tune within the effective range.
The effective range should be determined by the complete beverage system rather than MCC concentration alone. Almond solids, particle characteristics, mineral fortification, protein content, homogenization, thermal processing, and the target mouthfeel can all shift the level required for acceptable performance.
A useful way to evaluate MCC in almond milk is to separate raw-material effects from formulation and process effects. The exact test conditions should be adapted to the manufacturer’s equipment and product specification, but the following sequence provides a practical starting point:
The following framework is designed to separate raw-material effects from process effects during beverage development:
| Parameter | Example |
|---|---|
| Beverage | Almond milk |
| MCC system | Candidate colloidal MCC |
| Screening levels | 0%, 0.10%, 0.30%, 0.50% |
| Evaluation | Sedimentation, creaming, redispersibility |
| Process | Same conditions across trials |
| Storage | Day 0–30+ |
| Decision | Select lowest effective level |
Practical formulation note: If a laboratory sample stays stable but a commercial-scale batch develops sediment, don’t immediately increase MCC. First compare powder feeding, circulation, hydration time, homogenization pressure, and thermal processing between the two.
Cost per ton of beverage = MCC price/kg × MCC usage kg/ton
A lower ingredient price does not necessarily produce the lower formulation cost. Effective dosage, processing losses, any required CMC addition, and the resulting stability can all affect cost-in-use. (All figures are illustrative.)
Need help screening MCC grades for your almond milk? Share your almond solids level, target viscosity, and the stability problem you’re trying to solve.
Even an excellent grade underperforms when dispersion or hydration goes wrong. The failure chain is predictable: poor powder feeding leads to local over-concentration, which leads to agglomeration and incomplete hydration, which leads to weaker suspension performance. Controlled addition and uniform dispersion, by contrast, support adequate hydration and more reproducible functionality.
Visible dispersion is not the same as complete hydration. A powder may appear uniformly dispersed in the beverage while the MCC system is still developing its intended structure. Therefore, evaluate the material after the supplier-recommended hydration or activation period rather than judging performance immediately after powder addition.
Some colloidal MCC systems require controlled shear or activation after dispersion — the required shear level, hydration time, and addition sequence depend on the specific grade and the supplier’s instructions.
Watch these variables, starting from the supplier’s recommended procedure: powder addition point and feeding rate, mixing intensity and local concentration, hydration time and temperature, premixing strategy and ingredient order, and homogenization.
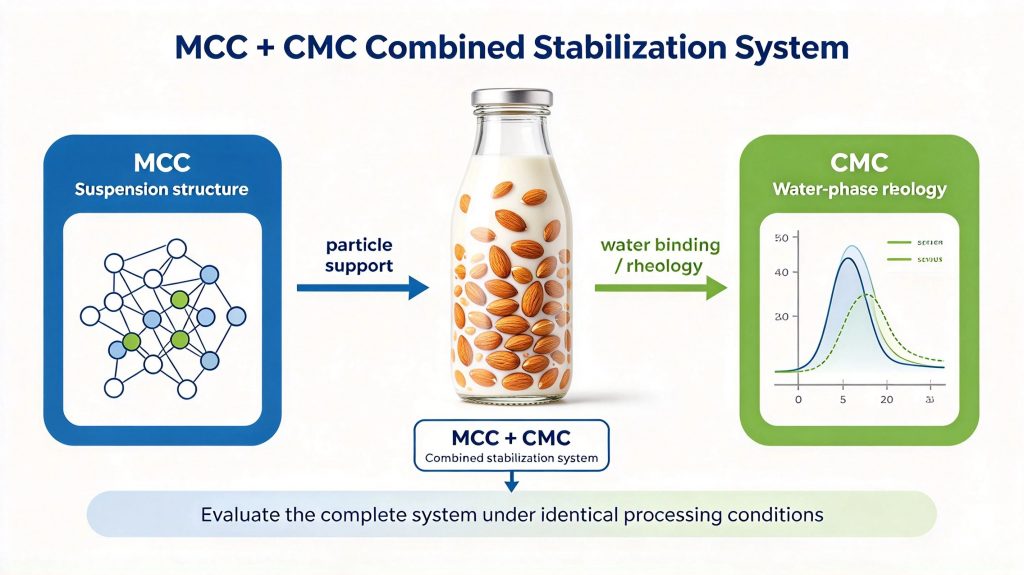
MCC and CMC should be treated as complementary components rather than interchangeable stabilizers. It primarily supports suspension structure, while CMC can modify continuous-phase rheology and water binding.
The combination can also raise viscosity and complexity, so test it rather than assume a multi-component system always wins.
| Trial | MCC | CMC | Objective |
|---|---|---|---|
| A | Low | Low | Light stabilization |
| B | Medium | Low | More suspension |
| C | Low | Medium | More water-phase support |
| D | Medium | Medium | Combined system |
| E | Higher | Low | MCC-dominant system |
| F | Low | Higher | CMC-dominant system |
Seek the lowest total stabilizer level that still delivers suspension, controlled rheology, acceptable mouthfeel, and storage stability. Some commercial colloidal MCC systems contain CMC, so ask the supplier to disclose the composition. When you approve a commercial formula, specify the actual MCC and CMC amounts or ranges.
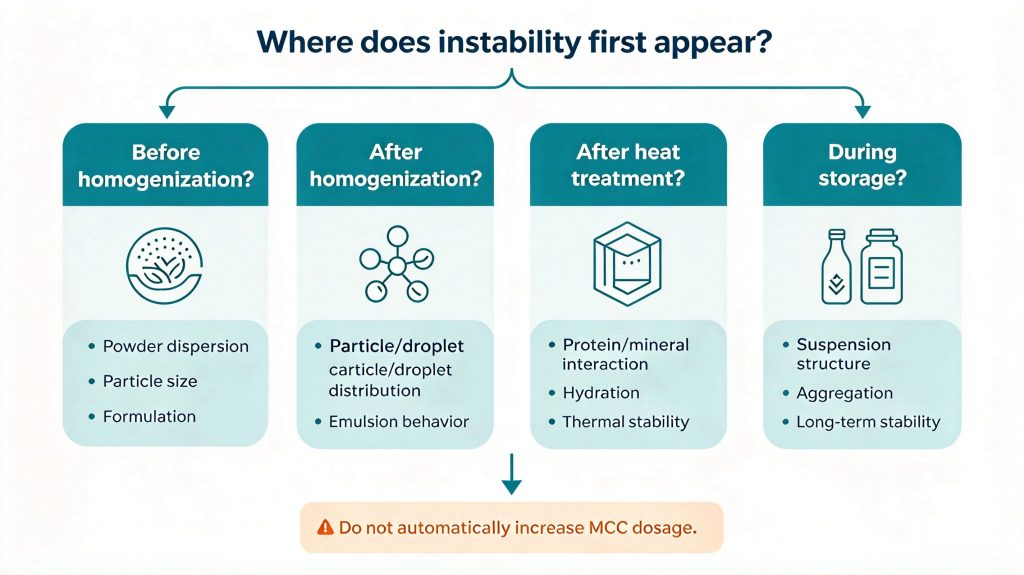
Rule 1 — Identify the likely cause before changing anything. Do not assume the MCC grade is the first variable to change. First identify when the instability appears, then control the main process and formulation variables so that individual changes can be evaluated clearly.
Rule 2 — The First-Failure-Point method. Where instability first appears points to the likely cause:
| Failure point | First variables to check |
|---|---|
| Before homogenization | Powder dispersion, particle size, formulation |
| Right after homogenization | Droplet/particle distribution, emulsion behavior |
| After heat treatment | Protein/mineral interactions, hydration, thermal stability |
| During storage | Suspension structure, aggregation, long-term stability |
Rule 3 — Don’t automatically add more MCC. Instability doesn’t always mean insufficient MCC. Use the table above to narrow down the likely cause before adjusting dosage.
Scenarios that need special care:
A formulation that looks excellent on Day 0 may still be poorly balanced if sedimentation, creaming, serum separation, or hard sediment develops later in storage. For this reason, early appearance should be treated as a screening result rather than proof of shelf-life stability.
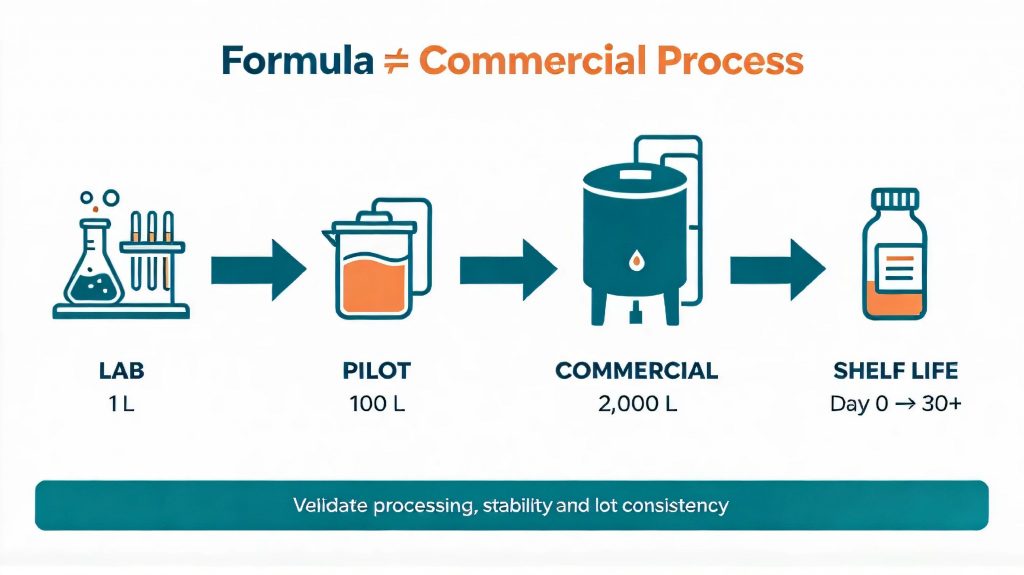
Start lab evaluation with a control without the MCC system. Track sedimentation, creaming, serum separation, rheology, sensory properties, and storage behavior at set intervals (Day 0, 1, 3, 7, 14, 30+). Use the same evaluation criteria and observation method across all trials so that results can be compared consistently. Test redispersibility separately — slight but compact sediment may deserve more concern than a larger amount of loose, easily redispersed sediment.
A single successful laboratory batch demonstrates feasibility, not commercial robustness. Repeatability should be confirmed across test batches and, where appropriate, across MCC production lots and pilot or commercial processing conditions.
Illustrative example — not a specific customer case.
| Stage | Volume | Observation |
|---|---|---|
| Lab | 1 L | Stable, good mouthfeel |
| Pilot | 100 L | Slight sediment appears |
| Commercial | 2,000 L | Visible sediment after storage |
Commercial scale-up is a process transfer, not a formula multiplication. When a formula behaves this way, investigate powder feeding, hydration, mixing, homogenization, and thermal processing before increasing the MCC dose.
Lot-to-lot qualification. Before a grade is approved for commercial supply, compare COA data, viscosity, moisture/LOD, and dispersion behavior across more than one production lot, alongside application performance in the customer’s own formulation. A formula that only performs well with one favorable lot is not yet considered commercially robust.
Define what “approved” means. Set minimum commercial requirements first, separate must-have requirements from nice-to-have improvements, and record the exact MCC grade, dosage, MCC/CMC ratio, addition and hydration procedure, homogenization parameters, and thermal process. Then confirm: Does the formula meet physical stability and sensory requirements? Does it stay stable after the intended thermal and storage conditions? Does it stay acceptable under normal lot variation? Can the supplier provide it consistently? Is it commercially viable on a cost-in-use basis?
Pre-launch and post-launch. Before launch, confirm the grade, dosage, and processing steps are documented and validated, and stability, sensory, and cost-in-use are approved. After launch, monitor viscosity, sedimentation, creaming, batch-to-batch variation, and MCC lot information. Treat any permanent formulation change as a controlled change that needs revalidation.
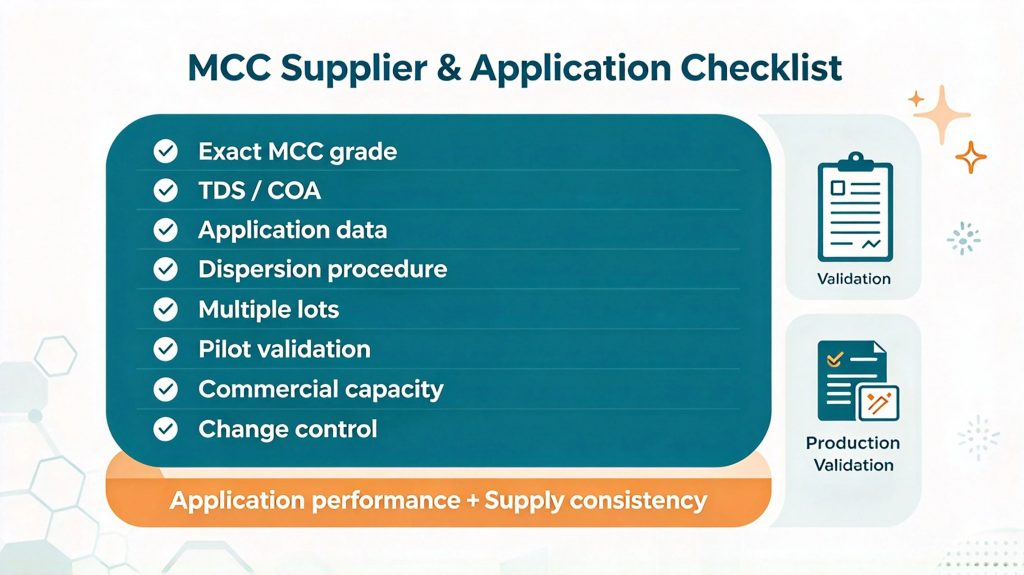
Supplier qualification should not end with confirming that an MCC meets a written specification. The material also needs to be qualified in the actual almond beverage application, because suspension performance depends on the full formulation and process — not the raw material alone. A grade that performs well in a simple laboratory dispersion may behave differently once almond solids, minerals, proteins, homogenization, and thermal processing are introduced.
| Information | Why it matters |
|---|---|
| Almond solids | Helps estimate particle load |
| Oil level | Helps distinguish suspension from emulsion issues |
| Protein level | Helps assess protein-related instability |
| Mineral fortification | Important for ionic interactions |
| Current stabilizer system | Prevents redundant recommendations |
| Processing route | Determines dispersion and thermal requirements |
| Current problem | Defines the initial troubleshooting direction |
| Target shelf life | Defines validation requirements |
You do not need to disclose your complete proprietary formula.
Use this matrix to compare candidate suppliers side by side.
| Qualification factor | What to check | Why it matters |
|---|---|---|
| MCC type | Ordinary / colloidal | Determines application functionality |
| CMC content | Exact composition | Affects formulation balance |
| Viscosity | Method + concentration | Enables meaningful comparison |
| COA | Multiple lots | Shows consistency |
| Application data | Beverage trials | Reduces trial risk |
| Dispersion | Recommended procedure | Affects performance |
| Manufacturing site | Actual site | Supports traceability |
| Lot-to-lot consistency | COA and application performance across lots | Confirms commercial robustness |
| MOQ | Commercial quantity | Affects purchasing |
| Lead time | Normal + peak | Supports production planning |
| Change control | Advance notification of specification, manufacturing-site, raw-material-source, or major process changes | Protects the validated formula |
| Problem | First check | MCC role | Other factor |
|---|---|---|---|
| Sedimentation | Particle size | Suspension | Homogenization |
| Creaming | Droplet size | Supportive | Emulsifier |
| Hard sediment | Aggregation | Structure | Minerals/protein |
| Too thick | Total hydrocolloid | Reduce/adjust | CMC/starch |
| UHT instability | Process | Validate | Heat treatment |
| Long-term separation | Structure | Optimize | Storage |
Manufacturers use MCC, especially colloidal MCC, to support suspension of insoluble almond particles, reduce visible sedimentation, and contribute to physical stability during shelf life.
Start by identifying whether the settling is caused by particle size, insufficient homogenization, poor stabilizer dispersion, incomplete hydration, or an unsuitable suspension system. Colloidal MCC can support suspension, but increasing dosage is not always the correct first step.
Because bulk viscosity alone does not fully determine suspension stability. Particle size, particle density, aggregation, rheology under relevant shear conditions, and stabilizer structure can all influence settling.
Yes, when the MCC grade, dosage, particle characteristics, dispersion, hydration, and processing conditions are appropriate for the formula. MCC can support suspension structure, but it cannot by itself correct excessively coarse particles or inadequate homogenization.
Colloidal MCC is an MCC-based system developed for aqueous dispersion and suspension applications. Depending on the commercial product, it may contain CMC or other formulation components that influence its dispersion and suspension behavior. Because composition and activation requirements vary by supplier, compare the actual technical specification and application performance rather than the product name alone.
There is no universally best grade across all almond beverage formulations. The best MCC is the one that meets your stability, sensory, processing, and cost-in-use targets in your own formula — screen at least two candidate grades under identical conditions.
No universal dosage exists. Some formulation programs may use a window such as 0.10%–0.50% for initial laboratory screening, then optimize based on suspension performance, mouthfeel, processing, and shelf-life results.
Yes. Compare MCC alone, MCC + low CMC, and MCC + moderate CMC under the same process to see whether CMC adds measurable benefit.
MCC may contribute to overall stability, but creaming differs from sedimentation. If a top layer persists, investigate oil droplet size and the emulsifier system first.
Common causes include an unsuitable grade, insufficient dosage, poor dispersion, incomplete hydration, large particles, inadequate homogenization, and mineral or protein interactions.
Yes. Calcium and protein fortification can change mineral interactions, protein behavior, rheology, and thermal response. Evaluate the complete formula under the intended homogenization, heat-treatment, storage, and end-use conditions rather than qualifying MCC separately from the finished beverage.
Confirm the exact grade, review the TDS and COA, test in your formula, validate at pilot scale, evaluate multiple lots, and confirm supply capacity and change control.
MCC selection should be based on the complete beverage system rather than the ingredient in isolation. A reliable development process connects application → MCC grade → dosage → dispersion → processing → stability → sensory performance → shelf life → supplier consistency → commercial validation.
For manufacturers evaluating colloidal MCC, MCC gel, or MCC + CMC for almond milk, ACTA can serve as a potential supply partner for application-oriented evaluation, sample testing, and technical discussion.
Need help selecting an MCC grade? Share your almond solids level, current stability problem, processing route, and target shelf life. You do not need to disclose your complete formula.
A successful MCC formulation is not simply a formula on paper. It is a validated system you can manufacture repeatedly.
About the Author
Richard Wang works with cellulose-based ingredients and supports international customers evaluating MCC, colloidal MCC, CMC, and related stabilizer systems for food and beverage applications. His work includes product selection, technical documentation, sample coordination, and application-focused communication with manufacturers and distributors.
