Pharmaceutical grade MCC (microcrystalline cellulose) is a widely used excipient in solid dosage formulations, particularly tablets and selected capsule formulations. Depending on the grade and formulation, it can function as a diluent, dry binder, and compression aid. However, the term “pharmaceutical grade” does not, by itself, establish compliance with a specific pharmacopoeia or prove suitability for every formulation.
Before selecting an MCC supplier, pharmaceutical manufacturers should verify five things: the exact product grade, applicable quality standards, batch-specific documentation, functional performance, and supply-chain controls. Even when two products meet the same basic monograph requirements, differences in particle-size distribution, moisture, density, and compaction behavior may affect processing and finished-tablet performance.
This guide explains how to evaluate pharmaceutical grade MCC, compare technical specifications, review supplier documents, assess samples, and prepare a more complete request for quotation (RFQ). It also covers excipient alternatives, supplier qualification, storage, and troubleshooting. The goal is not simply to find an MCC product with acceptable specifications, but to establish whether the exact grade, supporting evidence, formulation performance, and supply arrangements justify supplier approval.
| Factor | What to check | Why it matters |
|---|---|---|
| Product identity | Exact MCC grade and manufacturing source | Prevents comparing unlike materials |
| Applicable requirements | The relevant pharmacopoeial text and edition, applicable market requirements, and customer-specific specification | “Pharmaceutical grade” alone defines no limits |
| Documents | Specification, batch COA, TDS, SDS, and quality-system evidence for the quoted product and actual supply source | Supports qualification |
| Functional fit | Flow, compactibility, tablet or capsule performance | Compliance does not guarantee performance |
| Samples | Sample matches the exact grade and batch; evaluated against predefined criteria | Confirms suitability before commitment |
| Supply | Lead time, packaging, shelf life, change notification | Protects production planning |
| Commercial terms | Incoterms® rule and named place, payment terms, and total delivered cost on a comparable basis. | Exposes hidden costs |
Use this checklist to assess pharmaceutical grade MCC against the intended dosage form, applicable quality requirements, and planned manufacturing process.
Microcrystalline cellulose is a purified, partially depolymerized cellulose that formulators use widely in solid oral dosage forms. In practice, the phrase “pharmaceutical grade MCC” tells you that a supplier offers the material for evaluation as a pharmaceutical excipient. However, the phrase does not identify one universal product with identical properties across all suppliers.
Buyers should separate three related ideas:
For pharmaceutical grade MCC, the material name alone is not enough: qualification should be based on the exact grade, applicable specification, functional data, and intended use.
These ideas overlap, but they are not interchangeable. A statement that a product suits pharmaceutical use does not prove compliance with every pharmacopoeia, and it does not show that every customer-specific requirement has been met.
A batch-specific COA showing that the material meets defined quality requirements does not replace formulation testing. Likewise, successful performance in one tablet formulation does not remove the need to verify product identity, batch documentation, and continued suitability for the intended process.
MCC is not an active ingredient. Instead, it is an excipient that helps a formulation reach the required manufacturing properties, dosage-form structure, or product performance. Formulators evaluate it as a functional excipient for three main reasons:
For these reasons, the lowest-priced grade is not always the most economical. A cheap grade can cost more if it forces formulation adjustments, produces inconsistent tablets, or creates manufacturing problems.
Do not treat pharmaceutical grade MCC as interchangeable with industrial cellulose materials. Intended use, manufacturing controls, specifications, traceability, and documentation can differ, so compare the declared grade, compendial status, specification limits, and quality documentation before you buy.
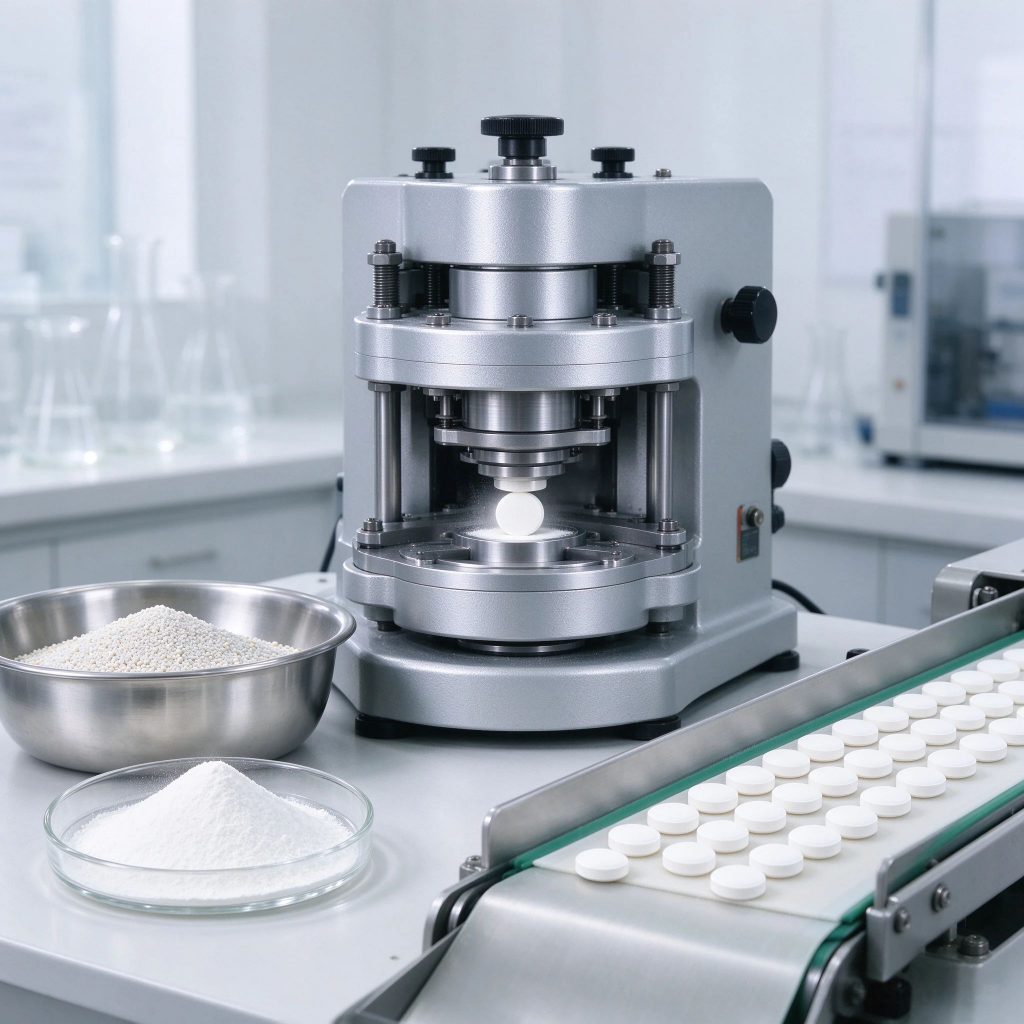
MCC serves several functions, depending on the grade and the formulation. Most often, formulators use it as a filler or diluent, a dry binder, and a direct-compression excipient. Because its role changes with the dosage form, you should understand the application before you compare grades.
| Application | Potential role of MCC | Key evaluation priorities |
|---|---|---|
| Direct-compression tablets | Diluent and compaction aid | Flow, compactibility, tablet strength, lubricant sensitivity |
| Wet-granulated tablets | Diluent and formulation component | Granule properties, drying, compression behavior |
| Hard capsules | Diluent or fill-blend component | Fill consistency, flow, content uniformity |
| Chewable tablets | Diluent and structural component | Mouthfeel, strength, friability |
| Orally disintegrating tablets | Diluent and structural component | Disintegration, strength, mouthfeel |
| Pellets and granules | Component in selected processes | Particle shape, size, strength, processability |
For example, a direct-compression tablet depends on powder flow and compact formation, while a capsule formulation depends more on filling consistency and blend uniformity. Therefore, a grade that performs well in one dosage form may not suit another. Likewise, a grade that works for conventional tablets may need separate evaluation for chewable or orally disintegrating products, where texture and breakup matter just as much as strength.
MCC also works as part of an excipient system. It may combine with lactose, mannitol, disintegrants such as croscarmellose sodium or sodium starch glycolate, lubricants such as magnesium stearate, and binders such as povidone. These combinations create trade-offs. Extra lubricant, for instance, can ease ejection but may weaken tablet bonding. Similarly, adding a disintegrant does not guarantee faster breakup if the tablet structure limits liquid penetration. Formulation work aims to balance these effects rather than maximize a single property.
Wet granulation may be selected when a formulation requires improved powder handling, blend uniformity, compactability, or other process characteristics that are difficult to achieve with direct compression alone.In that process, they mix powders, add a granulating liquid, dry the granules, and compress them. MCC can enter the formulation in the intragranular phase, the extragranular phase, or both. Intragranular MCC becomes part of the granule structure, while extragranular MCC joins the dried granules and can adjust the compression behavior of the final blend. These choices influence granule flow, blend compressibility, tablet strength, and disintegration. Therefore, confirm the split through controlled experiments rather than a universal rule. If hardness is inconsistent, check granule moisture, granule-size distribution, and binder performance first.
MCC can serve as a filler or diluent in the fill blend of hard gelatin or HPMC capsules, but capsule filling differs from tablet compression. Compact strength is not the main goal. Instead, the formulation must fill reliably, deliver consistent dosage units, and meet product performance requirements. Dosator and tamping-based systems handle powders differently, so evaluate the blend on the actual machine. If fill weight varies, review powder flow, segregation, machine settings, and the properties of the other ingredients as well as the MCC grade.
High-drug-load products leave little room for excipients, and the API may compact or flow poorly. MCC can help because of its compact-forming behavior. Nevertheless, adding more MCC does not automatically solve the problem, so the team must weigh the proportions of API, diluent, disintegrant, and lubricant. Low-dose products pose a different challenge. Blend uniformity matters more than total excipient mass, and differences in particle size, density, shape, and electrostatic behavior can cause segregation. MCC works as a diluent in these products, yet it does not guarantee content uniformity. For that reason, assess the order of addition, the mixing procedure, and transfer and feeding, and evaluate dosage units with the applicable methods. Supplier consistency also matters here, because small changes in excipient properties can affect a sensitive blend even within specification.
Direct compression is sensitive to powder flow, segregation, particle-size differences, and lubricant distribution. Poor flow can contribute to tablet-weight variation, while segregation can lead to content-uniformity problems. Inadequate compact formation may result in weak tablets or increased friability. MCC also shapes tablet structure and porosity, so it affects how liquid enters the compact and how it breaks apart; the full formulation and process decide disintegration and dissolution. Treat two common situations separately:
Before choosing a grade, define the main development objective. Ask:
Use these answers to identify the attributes that matter most during initial grade screening, and treat each candidate as unqualified until the required technical and quality assessments are complete.
Chewable tablets must combine mechanical strength with acceptable mouthfeel, taste, and ease of chewing. MCC can act as a diluent and structural component, but its effect on grittiness depends on grade, concentration, and particle properties, so evaluate strength and sensory properties together against predefined criteria. Orally disintegrating tablets add a different requirement: rapid breakup without losing handling strength, which depends on the disintegrant, porosity, compression conditions, soluble excipients, and API properties.
Formulators also use MCC in selected pellet and granule systems, including extrusion-spheronization. Here the evaluation covers pellet size distribution, shape, mechanical strength, and compatibility with later coating steps, so a grade chosen for tablets does not automatically suit pellet manufacture.
Grade names help you build a shortlist, but they do not replace specifications. Commercial MCC grades are often described by designations such as PH-101, PH-102, PH-200, PH-301, and PH-302. Use the following as a preliminary screening guide, and confirm every point against the supplier’s actual product data:
These are common screening ideas, not performance guarantees that every supplier provides. Reference values published in grade literature are informational and are not product quality standards. Do not copy numbers from another manufacturer’s documents; compare the verified specification and physical-property data for the exact grade you are considering, and then confirm performance in your own formulation.
The relevant attributes depend on the applicable monograph, the approved specification, and the intended formulation. Nevertheless, the following categories give procurement and technical teams a practical starting point.
Identity and purity. Identity tests confirm that the supplier delivers the specified substance, and purity requirements show whether the material meets the applicable limits. Always compare defined acceptance criteria. Generic phrases such as “high purity” replace nothing.
Moisture and loss on drying. Moisture can influence powder handling, blending, and compaction. However, the effect depends on the grade and the formulation, so a single moisture result does not predict every performance outcome. Define acceptance limits from the applicable specification and your own process requirements.
Particle size and distribution. Particle characteristics affect flow, blending, segregation, and compression. Two MCC products can satisfy the same basic chemical specification and still behave differently because their particle-size distribution or morphology differs.
Bulk density and flow. These properties influence hopper discharge, die filling, and tablet-weight consistency, particularly on high-speed presses. Bulk density, tapped density, and flow measurements describe different aspects of powder behavior, so no single value predicts die-filling performance in every formulation.
Functional performance. Ultimately, MCC performance depends on the grade, the formulation, and the process. A supplier’s typical values help with screening, but you must confirm suitability in your own formulation under representative conditions.A pharmaceutical grade MCC specification should clearly distinguish mandatory release limits from typical properties and actual batch results.
The first stage of evaluation confirms identity and reviews the applicable quality attributes. Depending on the governing specification, the review may include identification, loss on drying, residue on ignition, impurity limits, and other compendial requirements. Take the exact test list and acceptance criteria from the official standard and the approved product specification, not from a generic supplier description. Then check whether the COA reports actual results or only states that the material complies. Actual results give more useful information about batch consistency when you understand the method and specification. Finally, confirm that the material described in the COA matches the material quoted, sampled, supplied, and released for production.
Particle size affects flow, packing, blend uniformity, die filling, and compaction, but the relationships are not linear. A finer powder does not automatically make a better tablet, and a larger particle size does not guarantee better flow. In direct compression, consider particle size together with shape, porosity, bulk density, and the other ingredients. Ask each supplier:
Do not compare values from different suppliers when the methods differ. A grade that performs well on one line may behave differently on another with different feeders and speeds, so confirm whether the values are typical data or release specifications, which procedures produced them, and whether they stay consistent across batches. If flow is critical, add characterization and formulation trials.
For direct compression, MCC is valued for its ability to support compact formation. Still, distinguish three related ideas. Compressibility describes how a powder bed changes in volume under pressure. Compactability describes the ability to form a compact of a given mechanical strength. Tabletability links compaction pressure to tablet tensile strength. A grade that forms strong compacts under one set of conditions may behave differently when the formulation holds many other excipients, lubricant levels change, or compression speed rises. Treat a claim of “excellent compressibility” as an initial indication, not proof. A structured trial that measures tensile strength, friability, disintegration, ejection force where relevant, lubricant sensitivity, and performance across the pressure range tells you far more.
Loss on drying (LOD) and direct water-content measurements are not necessarily interchangeable, because the methods can measure different quantities. Therefore, confirm the test method and acceptance range in the specification before you compare suppliers, and ask whether the supplier monitors results across commercial batches. Remember too that a batch that leaves the factory within specification can meet different temperature and humidity conditions in shipping and warehousing. When you compare suppliers, first confirm that the methods are comparable, and then judge whether the difference is technically meaningful. Do not choose a product only because it reports the lowest LOD. Check that it consistently meets the specification and performs reliably in your process.
Excipient assessment may also include microbiological limits and other controls, depending on the intended use, the process, and the regulations. No single set of extra acceptance criteria applies identically to every pharmaceutical MCC application. Establish the requirements from the relevant pharmacopoeial provisions, the product specification, the customer requirements, and your risk assessment, and confirm which methods and limits apply.
One acceptable sample does not show that every shipment will perform the same way. Variation in particle size distribution, moisture, or density can affect powder handling and tablet production, and its practical impact depends on how sensitive your formulation is. Review COAs from several production batches where appropriate, compare the same attributes using equivalent methods, and confirm which attributes are release specifications and which are informational. In addition, ask how the supplier investigates out-of-specification results and communicates changes to raw materials, sites, or specifications. The depth of review should reflect how critical the excipient is to your product.
Start with the mandatory quality requirements: the pharmacopoeial, regulatory, and customer-specific criteria the material must meet. Then compare functional attributes, such as particle-size distribution, density, flow-related behavior, and compact formation, and review supply and documentation controls, such as traceability, COA availability, and change notification. A supplier with a detailed data package is not automatically better than one with a short specification sheet, but the detail affects how confidently you can assess compliance and consistency.
Separate mandatory acceptance criteria from typical physical-property data. Release specifications define the limits used to determine whether a batch meets the approved requirements. Typical values, by contrast, help buyers screen candidate grades but may not represent guaranteed limits for every batch.
For each important attribute, ask the supplier to identify the test method, acceptance criteria, and testing frequency, and to state whether the reported value is a release specification, a batch result, or typical informational data. This distinction is particularly important when comparing particle-size distribution, bulk density, moisture-related properties, and other attributes that may affect processing. Do not treat two grades as equivalent merely because their typical values look similar; confirm the applicable requirements and evaluate functional performance under comparable conditions.
Use the same specification basis for every supplier and record the source of every acceptance criterion. Do not compare a supplier’s typical values with another supplier’s guaranteed release limits as though they were equivalent. For each candidate grade, document:
Complete this comparison before selecting samples for formulation testing. If a candidate does not meet a mandatory requirement, do not use a favorable price or a promising preliminary trial to override that requirement.
Example. Suppose two suppliers both report particle size and bulk density. Supplier A lists the values as typical data, while Supplier B lists them as release limits with defined test methods. Check the test methods and the data classification first, and only then decide whether the numbers can be compared. Do not simply select the product whose values look more attractive.Typical values and release limits serve different purposes. If the data cannot be compared on the same basis, request additional information rather than ranking suppliers using the numbers alone.
MCC is an important excipient, but it is not the only option. Lactose, dibasic calcium phosphate, starch-based excipients, mannitol, and other materials can also act as diluents, fillers, or binders. Each has its own physical properties, processing behavior, and limits. Consequently, the best material depends on the API, the dosage form, the process, the target performance, and the applicable quality requirements. Compare specific commercial grades, not generic names, and judge them against the same criteria.
| Excipient | Typical role | What to compare with MCC |
|---|---|---|
| Lactose | Diluent; grades designed for direct compression or granulation | Tablet strength, flow, segregation risk, disintegration, API compatibility, cost |
| Dibasic calcium phosphate | Inorganic diluent with different density and compaction behavior | Bulk and tapped density, flow, compact formation, API compatibility |
| Pregelatinized starch | Binder, disintegrant, or diluent depending on grade | Degree of pregelatinization, disintegration, moisture behavior, compression |
| Mannitol | Diluent where solubility, taste, or mouthfeel matter | Mechanical strength, sensory performance, disintegration, stability |
| HPMC | Film coating, matrix release, capsule shells | Different function; not a direct substitute in conventional direct compression |
| Croscarmellose sodium | Superdisintegrant (crosslinked cellulose derivative) | Complements MCC; MCC does not replace a dedicated superdisintegrant |
MCC often earns evaluation when a formulation needs compact-forming capability or a multifunctional excipient. Lactose may fit when its grade-specific flow, compaction, or solubility suits the process. Neither is universally superior. Note also that lactose, as a reducing sugar, may need compatibility assessment with certain amine-containing APIs, depending on the formulation and stability data.
The two differ in density and compaction behavior, and density alone does not decide whether a blend will segregate or a tablet will pass. Assess API compatibility and any formulation-specific risks associated with the excipient’s chemical properties, moisture behavior, and processing conditions.
The materials overlap in some applications but are not interchangeable. Pregelatinized starch varies by degree of pregelatinization and function, so compare exact grades. Combining it with MCC can help when each contributes a different function, yet the combination may change compression, disintegration, and moisture sensitivity, so confirm it by controlled testing.
For chewable or orally disintegrating tablets, sensory requirements matter alongside strength. A formulation may even use both diluents, but determine the proportions experimentally.
Cellulose origin does not make excipients interchangeable. HPMC serves film coating, matrix, and capsule-shell roles. Croscarmellose sodium works as a superdisintegrant and differs from conventional sodium carboxymethylcellulose (CMC). Therefore, specify the exact excipient and avoid the broad term “CMC” without clarification.
Sometimes, but treat substitution as a formulation change, not a one-to-one purchasing decision. First, define the reason: cost, flow or feeding, tablet strength, disintegration or dissolution, supply, or a compatibility concern. Each goal needs its own evaluation. If the goal is cost, compare composition, yield, processing time, and quality as well as price per kilogram. If the goal is strength, confirm that disintegration and dissolution stay acceptable. For a marketed product, also assess change-control and regulatory implications. A substitute that passes a limited laboratory test or shares a similar description does not qualify for approval on that basis alone.
For an evidence-based final selection, define the dosage form and process, identify the main technical objective, compare documented specifications, run consistent formulation trials, and document the results with the appropriate qualification and change-control arrangements.
Pharmaceutical and food grade MCC may share the same basic chemical identity, yet they are not automatically interchangeable. A food-grade designation does not establish pharmaceutical suitability, and a pharmaceutical-grade designation does not demonstrate compliance with every food-market requirement.
| Evaluation factor | Pharmaceutical grade MCC | Food grade MCC |
|---|---|---|
| Intended application | Pharmaceutical formulations | Food products and permitted food uses |
| Applicable standards | Relevant pharmacopoeias and pharmaceutical requirements | Applicable food regulations and ingredient specifications |
| Batch documentation | Defined by applicable requirements and quality agreements | Defined by food regulations, specifications, and customer terms |
| Functional testing | Based on the pharmaceutical formulation | Based on the food formulation |
| Supplier qualification | Pharmaceutical risk assessment and quality procedures | Food-supplier approval and food-safety procedures |
| Substitution | Requires documented assessment and approval | Does not establish pharmaceutical suitability |
Because specifications, documentation, functional performance, and regulatory assessment can all differ, pharmaceutical manufacturers should not swap a food-grade material for a qualified excipient just to cut costs. A food-grade or pharmaceutical-grade name alone cannot replace verification of the requirements that apply to your market, and any proposed substitution must pass the manufacturer’s quality and change-control procedures.
This table is a general procurement framework. It does not claim that every pharmaceutical-grade product carries more documentation than every food-grade product. Actual requirements depend on the supplier, the market, and the customer agreement.
Potentially, but pharmaceutical suitability alone does not establish compliance with every food regulation. The material must also meet the requirements for the intended food use, including ingredient identity, purity, labeling, and conditions of use in the destination market, and the supplier should provide supporting documents. Suppliers that serve both pharmaceutical and food customers should therefore define product specifications, intended uses, and documentation separately for each market.
Pharmaceutical manufacturers should identify the compendial requirements applicable to the intended market and registered product, taking account of relevant laws, current official monographs, applicable general chapters, product filings, and customer-specific requirements.
Where compliance with USP–NF, the European Pharmacopoeia (Ph. Eur.), or the Japanese Pharmacopoeia (JP) is required or claimed, verify the applicable text and edition and obtain evidence that relates to the exact product grade and manufacturing source. Do not assume that compliance with one pharmacopoeia establishes compliance with the others, or that a general supplier statement proves that every customer-specific requirement has been met.
For Japan, confirm the applicable JP edition, effective dates, transitional arrangements, and any subsequent official corrections. JP19 was published on April 10, 2026, with immediate effect, and its transitional period ends on September 30, 2027. Buyers should consult the current official JP materials and applicable notices rather than relying on an older English translation or an earlier summary. Harmonized monograph status does not mean that every requirement is identical in every pharmacopoeia, so verify the exact text, edition, and local requirements for the intended product.
For official information, start with the primary sources. For USP–NF requirements, consult the current official monograph and applicable general chapters. Historical harmonization notices, such as the USP notice on the harmonized microcrystalline cellulose monograph, can provide background, but they should not replace verification of the current official requirements. EDQM maintains the European Pharmacopoeia, and PMDA publishes the Japanese Pharmacopoeia. The IPEC Federation also offers guidance on qualification of excipients (Version 3, 2026) and on GMP certification schemes for pharmaceutical excipients. Always check the current edition and the exact monograph text for your market.For pharmaceutical grade MCC, confirm the current official monograph and applicable edition for each target market rather than relying only on a supplier summary or historical harmonization notice.
Before qualification, ask suppliers to clarify:
Finally, remember that compendial compliance does not guarantee identical tablet performance. Two grades may meet the same monograph and still differ in particle characteristics, bulk density, flow, or compressibility. As a result, a supplier change or grade substitution needs functional comparison, not just a similar-looking COA.
A product can come with an acceptable COA and still raise questions about how the supplier manufactures, tests, documents, stores, and supplies it. Therefore, approach qualification as an ongoing quality-management process, not a one-time purchasing check. Industry groups such as the International Pharmaceutical Excipients Council (IPEC) and the Pharmaceutical Quality Group (PQG) publish excipient GMP and qualification guidance. These documents give useful frameworks, although the legal requirements that apply to you depend on your market and quality system.
Depending on the process and your risk assessment, relevant controls may cover:
Buyers should separate three claims that need different evidence: a supplier has a quality-management system, a supplier follows an excipient GMP guide, and a supplier holds a specific third-party certification. Do not assume that every pharmaceutical MCC supplier holds the same certificate, or that the phrase “GMP quality” proves compliance with a named certification standard. Ask which requirements the supplier follows and what evidence exists for the actual manufacturer, site, and product.
Traceability links a delivered lot to its manufacturing and testing history. You may need it to identify a batch, investigate a complaint, review a suspected defect, or assess a manufacturing change. Therefore, check that identifiers on the label, COA, shipping documents, and internal receiving records agree. Also remember that a supplier’s commercial office, a distributor, and the actual factory may be different entities. If your process requires the original manufacturer and site, document them and make sure they match the approved supply arrangement. When a distributor supplies the material, clarify who owns documentation, storage, traceability, and quality communication. This does not make every distributor unsuitable. It means the supply chain must deliver the transparency your use requires.
Do not assume that an approved grade stays identical in every relevant respect forever. Changes may involve raw-material sources, equipment, process parameters, analytical methods, sites, specifications, or packaging. Some have little impact, while others can alter physical properties, impurity profiles, or documentation. The key question is not whether changes are forbidden, but whether the supplier assesses, documents, communicates, and manages them under agreed requirements. A robust arrangement clarifies how the supplier identifies and assesses changes, which changes need notification, what data supports the assessment, who approves the change before use, and how qualification records get updated. For a marketed drug product, you must also assess regulatory implications, because a supplier’s notification does not decide whether a submission or other action is needed.
A quality agreement clarifies responsibilities among the manufacturer, distributor, and pharmaceutical customer. Typical topics include approved specifications, batch documentation, deviations and out-of-specification results, complaint investigation, change notification, traceability and record retention, recalls where applicable, and audit responsibilities. It does not replace testing or qualification, but it documents who does what. Confirm that the parties can actually fulfill the terms before you rely on them.
Not every supplier carries the same risk, so scale the qualification effort. Review four areas: material risk (are the required attributes defined, and could property variation affect your formulation?), manufacturing risk (do you know the actual source, and are process and quality controls documented?), documentation risk (are records complete, consistent, and traceable?), and supply risk (can the supplier maintain the approved product and communicate quality issues and changes promptly?).
Documents form the evidence base for supplier approval, but each one serves a different purpose.
A COA typically records the test results or conformity status for a defined material batch. Verify the reported information against the approved specification and the requirements agreed with the supplier. Check the following elements:
| COA element | What the buyer should verify |
|---|---|
| Product name and grade | Does it match the ordered MCC grade? |
| Batch or lot number | Does it match the packaging and shipment documents? |
| Specification reference | Does it identify the correct specification? |
| Test parameters and methods | Do they cover the required characteristics? |
| Results and limits | Do the values meet the applicable acceptance criteria? |
| Dates and release authorization | Does the document follow the supplier’s release process? |
| Traceability | Can you link the document reliably to the supplied batch? |
Compare each result with the approved specification, not with a range that merely looks reasonable. If a COA reports only “Pass” or “Complies,” decide whether that format meets your documentation requirements. Moreover, remember that one satisfactory COA does not prove that every future batch will match it.
A TDS describes general characteristics, typical properties, grades, applications, packaging, and handling advice. Separate formal specification limits from descriptive or typical values, because typical values do not act as guaranteed release limits.
An SDS covers hazards, handling, storage, and emergency measures. It supports safety assessment but does not replace a COA, compliance evidence, or a pharmaceutical quality assessment.
Confirm that the product name, grade, manufacturer identity, and specification basis are consistent across the quotation, TDS, product specification, and other applicable records. Separately verify that the batch or lot number on the COA matches the material label and relevant shipping or receiving records. Resolve discrepancies before relying on the documents for qualification or release.A documentation package for pharmaceutical grade MCC should link the approved grade and specification to the actual test results, material lot, and manufacturer or manufacturing site.
A document package is only useful if you read it critically. Ask five questions:
A single COA cannot establish complete supplier qualification either. It says little about manufacturing controls, contamination prevention, traceability systems, change management, or long-term consistency. Depending on risk, buyers also review approved specifications, quality-system information, manufacturing-site and supply-chain traceability, deviation and complaint procedures, change-control arrangements, and any audit results. The goal is not to collect the most documents. The goal is to obtain enough relevant evidence to support a documented decision.
Before you begin qualification, ask the supplier for a defined information package. A buyer-ready request includes:
Depending on your requirements, you may also request manufacturer and manufacturing-site identification, quality-management or excipient GMP certificates, composition or impurity statements, storage, transport, and retest or shelf-life information, quality agreements or supplier questionnaires, and relevant audit information. Not every document is mandatory for every product or market, so define the package from your regulatory framework and internal procedures. The IPEC Federation also publishes guidance on certificates of analysis for pharmaceutical excipients, which helps suppliers and users agree on what a COA should contain. When a COA looks inconsistent, ask the supplier’s quality contact for clarification, because A missing value, unclear test method, or inconsistent grade designation should be assessed and resolved according to its potential impact on product identity, specification compliance, and qualification decisions, even when the other reported results appear acceptable.
ACTA can confirm the product information, documents, and supply conditions available for a specific product and customer requirement. However, availability depends on the specific product, and each pharmacopoeial or quality-system claim needs supporting documents for that exact grade.
Not every gap carries the same risk. Classify each one:
A low price or an urgent delivery date never overrides a mandatory quality or regulatory requirement.
Start by defining your requirements. Before you contact any supplier, establish the dosage form, the manufacturing process (for instance direct compression or wet granulation), the applicable pharmacopoeial or customer requirements, the product specification and relevant physical properties, the documentation package, the expected volume and supply frequency, and the packaging, storage, and change-control requirements. When you share these details, suppliers can quote on a consistent basis. If you have not finalized the formulation, you can still request grade information for preliminary screening. However, do not approve the final grade until technical and quality processes confirm its suitability.
Neither channel wins in every situation. Buying from a manufacturer may offer direct communication about specifications, better access to manufacturing information, and a clearer path for change notifications and complaints. A qualified distributor may offer local stock, shorter delivery times, smaller quantities, and regional logistics. Still, a “factory-direct” claim does not replace product qualification, and a distributor does not automatically weaken traceability. Instead, clarify who owns technical documentation, batch traceability, and quality communication, and document the original manufacturing site where your quality system requires it.
Suppliers should not guarantee finished-tablet performance without understanding your formulation, process conditions, and acceptance criteria. If a supplier relies on phrases such as “high quality” or “excellent performance,” press for specifics.
A good supplier identifies the product clearly, states accurate specifications, and separates confirmed data from typical values and unverified claims. Base approval on the compliance questions in Section 6 and the information package in Section 7.Supplier qualification for pharmaceutical grade MCC should combine document review, representative sample testing, quality-system assessment, and change-control commitments.
Supplier qualification should proceed through defined stages, with clear evidence required at each gate. A favorable sample establishes only how the tested material performed under the evaluation conditions; ongoing suitability depends on the approved specification, batch records, quality controls, and change management.
Turn the workflow into a go/no-go process. A supplier moves to the next gate only after the current requirements are met.
| Decision stage | What to confirm | If the requirement is not met |
|---|---|---|
| Product screening | Specific grade, intended use, applicable standard | Clarify product identity first |
| Document review | Specification, batch COA, applicable quality records | Request missing documents or record the gap |
| Sample evaluation | Predefined physical and formulation performance criteria | Do not approve on a single strong result |
| Quality review | Traceability, change control, customer requirements | Resolve mandatory requirements before approval |
| Commercial review | Lead time, packaging, payment, shipping, total cost | Reassess on comparable terms |
| Final approval | Technical, quality, and purchasing approvals complete | Record the approved scope and any limitations |
Group the criteria in three tiers so that the decision follows a clear order:
The scorecard compares suppliers that have passed the gates. A decision record, by contrast, documents the approved scope, the unresolved issues, and the final decision. Record:
The scope depends on the supplier’s role and your risk assessment. A useful audit examines quality management (specifications, document control, deviations, complaints, corrective actions), manufacturing and process controls at the actual site, laboratory and testing controls, and traceability and change control. It should also end with documented findings and agreed corrective actions. An audit is not a checklist exercise. Its value lies in showing whether the supplier’s controls suit the relationship and whether the supplier has addressed identified risks.
A red flag does not automatically disqualify a supplier. It tells you to collect more evidence before you decide.
A weighted scorecard keeps comparisons consistent. Adjust the illustrative weights below to your quality system and priorities.
| Evaluation category | Illustrative weight |
|---|---|
| Product specification and applicable compliance | 25% |
| Quality documentation and traceability | 20% |
| Functional suitability and technical support | 20% |
| Supply reliability and lead time | 15% |
| Total delivered cost | 10% |
| Packaging and logistics | 5% |
| Communication and change management | 5% |
| Total | 100% |
Rate each category on a consistent scale, such as 1 to 5. Calculate each weighted contribution by multiplying the category weight by the assigned rating divided by the maximum rating of 5. Apply mandatory quality and compliance criteria as pass/fail gates before calculating the comparative score, and never let a high total override a critical failure.
Comparing pharmaceutical MCC quotations takes more than comparing price per kilogram. Offers may differ in grade, specifications, manufacturing source, packaging, order quantity, delivery terms, and documentation. To make a fair comparison, ask every supplier to quote against the same requirements.
| Comparison factor | What the buyer should confirm |
|---|---|
| Product identity | Exact MCC grade and manufacturing source |
| Quality requirements | Applicable specifications and compliance evidence |
| Technical properties | Relevant physical characteristics and test methods |
| Documentation | COA, TDS, SDS, and other required records |
| Packaging | Pack size, materials, labeling, and palletization |
| Order quantity | Minimum order quantity and volume-based pricing |
| Delivery terms | Incoterms® rule, named place, freight responsibilities, and schedule |
| Supply continuity | Lead time and repeat-order arrangements |
| Payment terms | Payment schedule, currency, and transaction conditions |
| Change management | Notification and approval arrangements |
Confirm whether each quotation includes freight, insurance, duties, taxes, and other applicable charges. For international purchases, specify the correct Incoterms® rule and named place.
A lower FOB price does not necessarily mean a lower delivered cost. Freight, insurance, customs expenses, and other import-related charges can significantly affect the final purchase cost.
No single price applies to every pharmaceutical MCC product. Pricing depends on factors such as grade, order volume, manufacturing source, specification requirements, packaging, destination market, and commercial terms.
Request a current quotation for the exact grade and delivery arrangement required. Avoid treating an isolated quotation as a reliable market benchmark unless the product specifications and commercial conditions are comparable.
A complete purchasing assessment may include:
Not every cost applies to every purchase. Nevertheless, evaluating the total cost helps buyers identify differences that a unit-price comparison may overlook.
First, confirm that every candidate meets the essential technical and quality requirements. A lower-priced product that fails these requirements is not a valid equivalent. A higher price is not automatically better, and a lower price is not automatically risky. The final decision should be based on documented suitability, comparable quotations, and the complete commercial arrangement.
A sample often forms the first step in evaluating a candidate grade. However, a request without clear criteria produces inconclusive results. Before the supplier ships anything, decide what the sample must show. Do you want to review powder properties, screen a formulation, compare compact formation, or start a formal qualification? Each purpose needs different quantities, documents, and tests.
The sample label and documents must let you identify the material and link it to the relevant quality records. If the sample feeds a formal qualification, follow your established sampling, testing, and approval procedures. A preliminary trial never counts as final approval.
First, review the paperwork and confirm that the identity, grade, and batch information agree. Resolve any discrepancy before you test. Second, decide which attributes matter for your application, such as specification parameters and physical properties. Third, test under controlled conditions that suit the formulation and process.
For a direct-compression tablet, the study may examine powder handling, blend behavior, tablet strength, friability, and disintegration. For a capsule, it may focus on filling consistency and blend uniformity. Your technical and quality teams should set the plan, because not every attribute needs measuring in every application and no generic test replaces full qualification.
Avoid changing too many variables at once. When you compare two grades, hold the formulation and processing conditions as constant as reasonably possible. If you change the grade, lubricant level, mixing time, and compression pressure together, you cannot tell which factor caused the result. Where you must study several factors, use a scientifically justified experimental design and record the conditions of every run.
Also evaluate more than one attribute. A sample that makes stronger tablets is not the best choice if disintegration becomes unacceptable or handling suffers. Likewise, a grade with good flow may still need review if compact formation falls short. Look for a suitable overall balance instead of optimizing one measurement.
A vague request for “pharmaceutical MCC price” produces quotations you cannot compare. A complete request for quotation (RFQ) lets suppliers identify a suitable product and quote accurately. Share only the technical and commercial information the evaluation needs, and protect confidential formulation details.
Use the RFQ in three stages:
Subject: RFQ for Pharmaceutical Grade Microcrystalline Cellulose (MCC)
Dear Sales Team,
We are evaluating pharmaceutical grade microcrystalline cellulose for our excipient sourcing program. Please send your quotation and technical information for the grade best suited to our application.
Please also tell us whether you manufacture this grade yourself, which physical-property data you can share, and how you notify customers of changes.
Best regards, [Name, company, country, email]
If you are replacing an existing grade, attach your current specification so suppliers can judge whether their product is a suitable candidate. Do not assume that a grade with a similar name is technically equivalent.
Pharmaceutical MCC sourcing works best as a controlled supply-chain process, not a series of isolated purchase orders. For an established formulation, an unplanned grade or supplier change involves far more than a purchasing substitution.
Watch for six risks, and match each with a control:
| Risk | Risk-control approach |
|---|---|
| Unclear product identity | Specify the exact grade, specification, and documents in the purchasing and qualification process |
| Unsupported compliance claims | Request the specification and supporting documents, and confirm they apply to the exact grade and source |
| Inconsistent batch performance | Review batch data, monitor incoming results, and trend them where risk justifies it |
| Unexpected manufacturing or specification changes | Define notification, impact assessment, and approval in a quality agreement |
| Shipping or inventory disruption | Assess lead times, packaging, storage, inventory cover, and contingency plans |
| Overdependence on one source | Evaluate whether a second source suits the product |
A second source improves resilience, but it does not remove risk automatically. Consider how important MCC is to the formulation, how reliable the current source is, how long a replacement evaluation takes, how specifications and physical properties differ, and what regulatory assessment the change needs. If you decide to qualify a second supplier, start before a supply emergency. Also remember that two products carrying the same generic name are not interchangeable until you establish the evidence for your intended use.
Record quality responsibilities in a quality agreement (see Section 6), and put commercial terms such as grade, quantity, packaging, delivery, forecasting, and confidentiality in the supply agreement.
After approval, keep three habits. Make quotations and purchase orders consistent, so that the grade, quantity, packaging, and delivery terms match before shipment. Assign clear owners for change notifications and complaints. Track supply performance continuously.
Excipient quality depends on how the material is packaged, shipped, stored, and handled, not only on how it left the factory. Even a batch that met its release specification can raise concerns after moisture exposure, packaging damage, contamination, or a loss of traceability. Follow the supplier’s approved documentation and your own quality procedures, because no single storage instruction suits every grade, supplier, and package.
Keep MCC in its original packaging until use when practical. Protect packages from damage, water, condensation, and contamination, and keep storage areas clean and segregated. Apply an approved stock-rotation method, such as first-expired, first-out. If water exposure or an unknown storage history affects a package, place the material on hold. Do not dry it as an improvised fix, because that treatment can introduce new risks and does not address contamination or other changes.
Confirm the configuration before you order: net weight, outer packaging, liner arrangement, closure and sealing, labeling and batch identification, palletization, and export packaging. Do not assume that all suppliers use the same format. For international shipments, also check that the packaging suits the planned route and warehouse conditions.
These terms are related, but they are not interchangeable. Shelf life describes the period during which the material is expected to stay suitable under specified conditions. A retest period marks when you must retest the material before deciding on continued suitability. Meanings differ between quality systems, so ask the supplier what each term means in its documents. Never assume an industry-wide value. Request the assigned period, the date from which it runs, the storage conditions, and, for large or long-lead-time orders, the minimum remaining shelf life at delivery.
Verify product identity against the order, check lot identification against the documents, inspect packaging for tears, water damage, and broken seals, review the documents, and keep the material under hold status until the required release steps finish. A good packaging inspection does not replace sampling, testing, or quality approval.
Transit adds risks that a specification never shows. Agree on product grade, lot identification, packaging, documents, and a procedure for reporting transit damage before shipment. Do not assume that temperature-controlled transport is either required or unnecessary for every MCC grade. Base the decision on the supplier’s documentation, packaging, route risks, and applicable quality requirements.
Balance lead time, expected consumption, warehouse capacity, release lead time, and shelf-life information. Excess stock increases storage time, while too little stock exposes production to supply delays.
Common formats for powdered excipients include multi-layer bags, bags with inner liners, and bulk packaging. The number of layers alone does not prove suitability, so confirm the packaging materials, closure system, and intended protection. For a liner, clarify the material, closure method, and integrity expectations. Larger formats may suit high-consumption sites with proper handling equipment, but they cost more in practice if the material is consumed slowly or the site cannot manage partly used packages.
Once a bag is open, the remaining material faces different exposure. Your procedure should cover identification of the opened package, preservation of the original lot number, documentation of the opening, protection against contamination and moisture, resealing or transfer to approved packaging, storage conditions and duration, and disposal or reassessment when required. Do not transfer material to an unapproved container without considering identification, contamination control, and traceability. If you cannot reliably identify the remaining quantity or its handling history, assess it under the quality procedure before further use.
The answer depends on the applicable documentation, quality system, and regulatory requirements, not on a general industry assumption. A retest date does not prove that the material has failed, and passing a few tests does not prove that every relevant attribute remains acceptable. Where your procedure permits reassessment, follow it, document the decision, and let the responsible quality function release the material.
A suitable MCC grade can still produce poor results when the formulation, blending, compression settings, or storage conditions fall out of control. Therefore, do not blame MCC automatically. The active ingredient, other excipients, lubricant level, moisture, equipment, and manufacturing history all contribute. A structured process works best: define the failure, verify the result, review recent changes, compare material records, test plausible causes one at a time, and document the conclusion.
| Observed problem | Possible contributing factors | Initial investigation |
|---|---|---|
| Low tablet hardness | Compact formation, lubrication, compression settings, formulation balance | Review hardness data, lubricant conditions, and compression records |
| High friability | Weak bonding, formulation issues, compression defects | Review tablet appearance, friability results, and process conditions |
| Poor powder flow | Particle characteristics, moisture, blend composition, equipment | Assess the blend and feeding system; review physical data |
| Tablet weight variation | Feeding instability, segregation, die filling | Review weight trends, blend behavior, and machine settings |
| Delayed disintegration | Tablet structure, compression, disintegrant system, lubrication | Compare hardness, disintegration, formulation, and process records |
| Slow dissolution | API properties, tablet structure, formulation or process changes | Review dissolution data and plausible causes |
| Sticking or picking | Adhesion, moisture, lubrication, tooling condition | Inspect tooling, storage conditions, blend, and compression settings |
| Capping or lamination | Air entrapment, elastic recovery, tooling, formulation | Characterize the defect and assess compression and material behavior |
| Batch-to-batch variation | Raw-material variation, process changes, testing differences | Compare batch records, COAs, process parameters, and history |
Use this table for initial classification only. Your deviation, investigation, and corrective-action procedures decide the actual response.
Two cautions apply across all problems. First, do not raise MCC concentration or compression force indefinitely to fix hardness or friability, since higher pressure can affect porosity, disintegration, and dissolution. Second, remember that hardness and dissolution are different measurements, so a change in one does not predict the other.
Consider a grade change only when the investigation shows that a material property contributes meaningfully to the problem and an alternative has a reasonable technical basis. Support the change with comparative testing, supplier qualification, and a regulatory assessment.
Seven mistakes to avoid
Before approving an MCC supplier, confirm the following points according to your product requirements and quality procedures.
Product requirements
Documentation and quality
Technical evaluation
Commercial and supply approval
This checklist supports supplier evaluation; it does not replace the applicable quality system, regulatory assessment, or formal product-approval process.
Pharmaceutical grade MCC is microcrystalline cellulose offered for use as a pharmaceutical excipient, subject to the applicable requirements and your qualification process. The term describes intended use; it does not by itself identify a specific specification or prove compliance with any pharmacopoeia.
No. Compliance with each standard needs explicit evidence for the exact grade. If your project needs more than one pharmacopoeia, ask the supplier to confirm each requirement.
No single grade suits every formulation, so evaluate candidates against your own criteria. Compare candidates on powder flow, compactibility, tablet strength, friability, disintegration, dissolution, lubricant sensitivity, and batch consistency, and confirm the result at pilot or commercial scale where appropriate.
Request a product specification, a COA, a TDS, an SDS, and any quality-system, compliance, shelf-life, storage, and change-control information your quality system requires. Receiving a document does not prove that the product meets every pharmaceutical requirement.
Not automatically. Two grades can share a chemical identity yet differ in properties that affect blend uniformity, tablet strength, friability, disintegration, and dissolution. Compare the specifications, test the candidate, and follow change control.
Grade, specification and documentation requirements, manufacturing source, order quantity, packaging, shipping route, payment terms, and supply availability all play a role. Request quotations for the same specification and delivery basis, and compare total delivered cost.
Review COAs from several production batches against the same specification and test methods, and ask which attributes are release specifications. Compare the physical properties that matter for your process. For critical products, add comparative formulation testing and monitor incoming results over time.
State the application and dosage form, the required grade or specification, the applicable standard, the documents you need, sample and annual quantities, packaging, destination, and Incoterm. Say whether you are replacing an existing grade, and attach your current specification when possible.
No. The applicable acceptance criteria depend on the relevant pharmacopoeial requirements, the approved product specification, the intended market, and any additional customer requirements.
When comparing pharmaceutical grade MCC suppliers, request the specification for the exact grade and verify the applicable test methods and acceptance criteria. Distinguish guaranteed release limits from typical physical-property data, and review the relevant COA against the approved requirements. Generic online ranges should not be treated as universal release specifications or proof of compliance.
PH-101-type grades are often screened when finer particle characteristics are relevant, while PH-102-type grades are commonly evaluated for direct-compression applications where powder flow and compactability both matter. PH-200-type grades are generally coarser in commonly used commercial grade families. These descriptions are preliminary selection guidance only; confirm the exact manufacturer’s specification and functional data before choosing a grade. Specific values depend on the manufacturer and the approved specification, so compare verified data for the exact grade.
Reliable pharmaceutical MCC sourcing balances technical suitability, documented quality, commercial transparency, and supply continuity. A robust process starts with a clear specification, evaluates the supplier’s evidence, confirms performance through testing, and sets up ongoing quality and supply management. Price matters, but it comes after you define the essential technical and quality requirements.
Key takeaways
Before requesting a quotation, confirm that the offered MCC grade, applicable quality requirements, supporting documents, and supply conditions match your intended application.
Qingdao ACTA Biotechnology Co., Ltd. can review your requirements and confirm which product information, technical documents, samples, and commercial options are available for your inquiry. After you submit an inquiry, we will confirm whether the requested grade can be supplied, which technical documents are available, whether samples can be arranged, and which requirements still need further confirmation. Availability and compliance claims must be verified for the exact product and manufacturing source.
To help us assess your request, please provide the intended dosage form, applicable specification, required documentation, sample quantity, estimated annual demand, destination country, and preferred delivery terms.
Email: wangpengfei@actabiotechnology.com
WhatsApp: +86 182 6365 3583
A general product description or preliminary sample does not, by itself, establish pharmaceutical suitability.
This guide provides general information for supplier evaluation. Specifications, regulatory requirements, and test methods vary by grade, region, and application. Always confirm applicable requirements with the relevant standards, your quality procedures, and the supplier’s current documentation before purchasing or using an excipient.
These sources describe the relevant standards and guidance frameworks. Confirm the applicable edition, effective date, and transitional arrangements using the current official texts for your market and product, rather than relying solely on previews, summaries, or earlier harmonization notices.
