ACTA Industry | September 21, 2026 | Beverage Stabilizers–Protein drink stabilizers
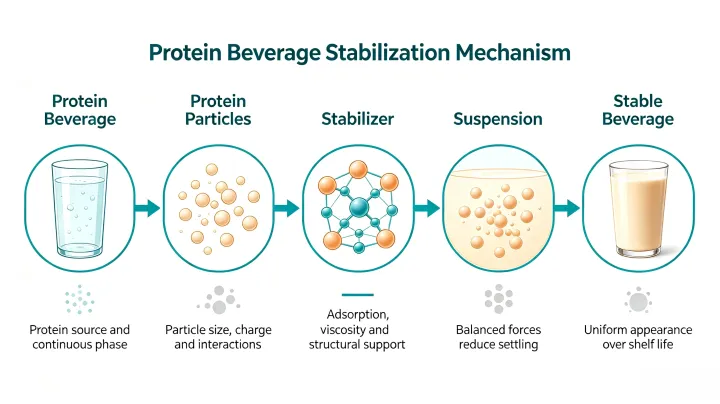
Protein drink stabilizers play a critical role in maintaining physical stability, texture, suspension and consistency in high-protein beverages. Unlike conventional drinks, protein beverages can develop sedimentation, protein aggregation, creaming, phase separation, excessive viscosity or poor redispersion because proteins interact with minerals, fats, carbohydrates, salts, pH, heat and processing conditions. Choosing the right protein drink stabilizers therefore requires more than selecting a thickener—it requires matching the stabilizer system, grade, dosage and processing conditions to the specific beverage matrix.
Consequently, protein drinks can show a wide range of stability problems: protein sedimentation, mineral-protein aggregation, creaming, phase separation, excessive viscosity, thin or weak body, gritty or chalky mouthfeel, poor redispersion, ring formation on the bottle neck, and gradual appearance changes over shelf life. Because of this, selecting protein drink stabilizers should never be treated as simply picking a thickener. A workable system has to match the beverage’s protein source, solids content, pH, mineral profile, processing conditions, target viscosity and required shelf life all at once.
This guide walks through how to evaluate protein drink stabilizers from a formulation and manufacturing standpoint: what they do, why protein systems behave differently from ordinary beverages, how to compare MCC, CMC, xanthan gum and modified starch, how to troubleshoot instability, how dosage and processing interact, how application context changes the strategy, how to validate stability and scale up, and how to qualify a supplier.
If your protein beverage develops sediment after 7–30 days, becomes too viscous after stabilizer addition, separates after UHT processing, or shows poor redispersion after storage, this guide provides a structured approach to identify the likely mechanism and screen an appropriate stabilizer system.
This technical guide helps R&D, formulation, procurement and quality teams develop protein-containing beverages. It presents formulation-screening principles rather than universal specifications, so development teams should validate the final ingredient selection, dosage and processing conditions in the target beverage matrix.
Author: ACTA Technical Team
Technical Reviewer: ACTA Technical Team — Food Hydrocolloids & Beverage Applications
Last Updated: September 2026
Scope: This guide focuses on physical stability and formulation screening for protein-containing beverages. It does not replace product-specific regulatory, microbiological, nutritional or shelf-life validation.For a broader overview of hydrocolloid functions and formulation considerations, see our Food Hydrocolloids Guide.
Table of Contents
Protein drink stabilizers are functional ingredients, or ingredient systems, used to improve the physical stability, texture and consistency of protein-containing beverages. Depending on the formulation, a stabilizer system can support several functions at once: suspending insoluble or slowly settling particles, controlling sedimentation, supporting protein dispersion, managing viscosity and body, improving emulsion stability, reducing phase separation, maintaining consistent mouthfeel through storage, and improving redispersion after the product has stood undisturbed.
Common Stabilizer Components in Protein Beverages
| Ingredient | Primary Functional Role |
|---|---|
| Colloidal MCC (commonly used in MCC Gel-type beverage stabilization systems) | Suspension structure for protein-containing particles and insoluble components |
| CMC (sodium carboxymethyl cellulose) | Viscosity, water binding, water-phase stability |
| Xanthan gum | Viscosity and shear-thinning rheology |
| Modified starch | Body, texture and formulation structure |
| Carrageenan | Protein interaction and gelling in selected dairy-protein systems |
| Pectin | Protein stabilization in suitable acidic (low-pH) systems |
These ingredients do not perform the same function, and treating them as interchangeable is where many formulations go wrong. Raising viscosity can slow the movement of suspended particles, but a beverage that becomes too thick no longer delivers the drinking experience consumers expect. A gum can provide strong thickening yet be the wrong choice when the target is suspension at a relatively low finished-product viscosity. Because of this, stabilizer selection should start from the failure mechanism, not from an ingredient name — a principle that runs through every section of this guide.
ACTA Technical Insight: Suspension Is Not the Same as Viscosity A protein beverage can become more viscous without achieving the desired suspension stability. During formulation screening, ACTA recommends evaluating sedimentation behavior and finished-product viscosity as separate variables. This helps formulators identify whether the formulation needs stronger suspension structure or simply more water-phase viscosity. A higher-viscosity beverage is not necessarily a more stable beverage — stability should be evaluated through sedimentation, particle movement, redispersion and finished-product rheology rather than viscosity alone.
Protein Drink Stabilizer Selection Flow
What is the main problem?
        ↓
Sedimentation?
  → Check protein/mineral aggregation and particle size
  → Screen colloidal MCC / CMC

Creaming or phase separation?
  → Check fat/oil content and homogenization
  → Evaluate an emulsion-focused system

Excessive viscosity or gummy texture?
  → Review total stabilizer dosage and grade
  → Screen a lower-viscosity grade or reduce total dosage

Gritty or chalky mouthfeel?
  → Check protein particle size and hydration
  → Review processing before changing the stabilizer

Poor redispersion after storage?
  → Check sediment structure, not just sediment volume
  → Evaluate a suspension-oriented system
This flow is a starting point for screening, not a substitute for the mechanism-by-mechanism troubleshooting in Section 4.
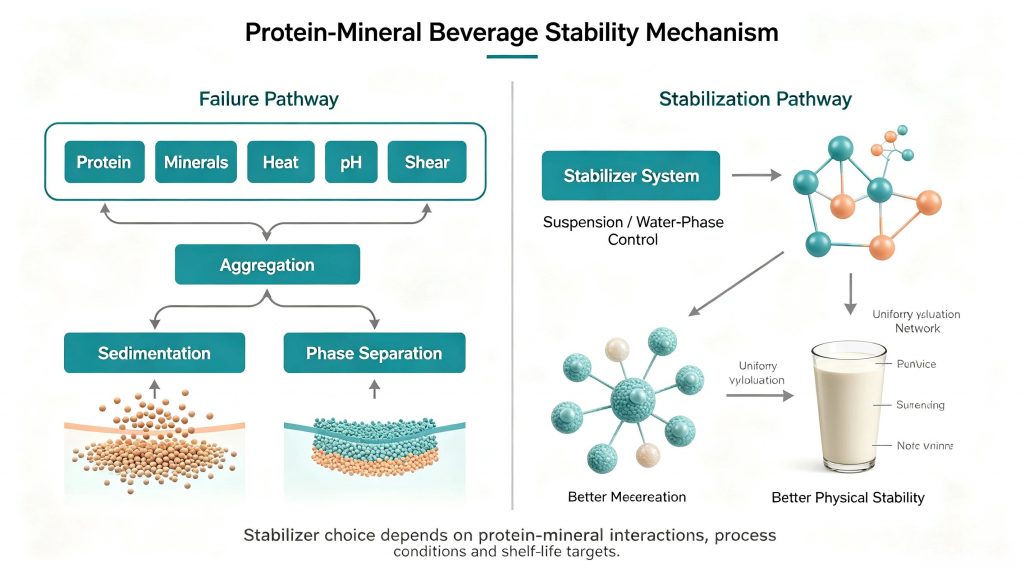
Protein beverages are more difficult to stabilize than many conventional beverages because protein interactions can change with pH, ionic strength, temperature and processing history. These factors can influence protein aggregation, particle interactions and the physical stability of the finished beverage.
Higher protein content raises formulation sensitivity. As protein concentration increases, the system becomes more sensitive to interactions with calcium, phosphate, salts, sweeteners, oils and flavors, all of which can affect dispersion, viscosity and particle behavior. As a result, the stabilizer system has to work within the complete formulation rather than in isolation, since a grade that performs well in a simplified bench trial can behave differently once every other ingredient is present.
Thermal processing changes protein behavior. Most ready-to-drink protein beverages require pasteurization or UHT treatment for commercial shelf life, and heating can alter protein conformation and protein-protein interactions. Consequently, a stabilizer that performs well in an unheated laboratory sample does not automatically deliver the same result after commercial-scale heat treatment — the finished-process sample, not the cold bench trial, is the one that matters.
Storage time is part of the test, not an afterthought. Because instability can develop gradually, a useful development program tracks the beverage across multiple time points rather than a single Day-0 check.
| Evaluation Point | What to Observe |
|---|---|
| Day 0 | Initial dispersion, viscosity and appearance |
| Day 7 | Early sedimentation or phase changes |
| Day 14 | Particle movement, creaming and texture |
| Day 30 | Long-term physical stability |
| Extended storage | Shelf-life behavior under intended distribution conditions |
The exact schedule should be adapted to the product’s intended shelf life and storage conditions, but the underlying principle stays the same: track trends across time, not a single snapshot.
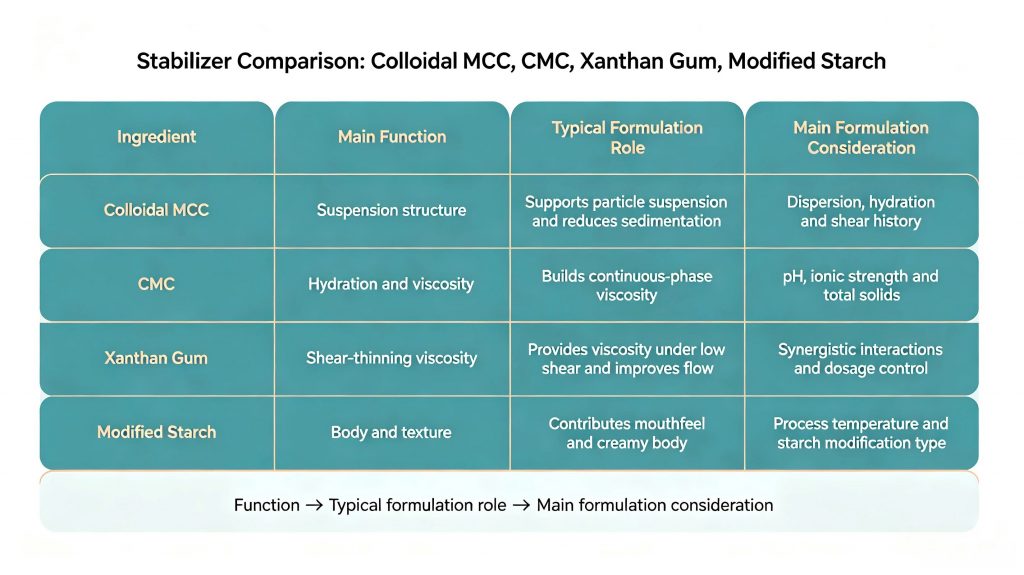
Different protein drink stabilizers provide different functional effects, so ingredient selection should begin with the stability problem rather than with a single preferred ingredient.Because protein beverages rarely fail for just one reason, the comparison below focuses on what a formulator or purchasing team actually needs to decide between: suspension versus thickening function, texture impact, processing considerations, and when a combination makes more sense than a single ingredient.
| Stabilizer | Primary Role in Protein Drinks | Typical Formulation Question |
|---|---|---|
| Colloidal MCC | Suspends protein and mineral particles without relying on bulk viscosity | Can the beverage stay suspended without becoming too thick to drink? |
| CMC | Viscosity, hydration support and water-phase control | Does the system need more body or better water-phase stability? |
| Xanthan gum | Viscosity and shear-thinning rheology | Does the beverage need stronger flow control or pourability at rest? |
| Modified starch | Body, texture and mouthfeel structure | Does the product need a creamier, more structured mouthfeel? |
Increasing viscosity is often considered the easiest way to improve stability. However, viscosity alone does not guarantee a stable protein beverage. A highly viscous drink may still suffer from sedimentation, poor redispersion or processing difficulties.
Raising viscosity often seems like the easiest way to improve stability, but higher viscosity does not necessarily deliver better stability. Excessive viscosity can create additional formulation and processing problems: a protein drink may remain suspended but become too thick to drink, difficult to fill, pump or homogenize, or unpleasant in the mouth. The real target is functional stability at an acceptable finished-product viscosity, which makes a structured combination system useful in many formulations.
Formulators can evaluate a colloidal MCC and CMC system when the formulation requires both suspension structure and water-phase viscosity or hydration support. Colloidal MCC contributes suspension structure, while CMC supports hydration, viscosity control and water-phase behavior. However, formulators should establish the appropriate ratio and dosage through trials that reflect the specific formulation and process rather than applying a recipe from another product.For a more detailed discussion of MCC in beverage suspension and cloud stability, see our guide to MCC for Cloud Stability.
| Grade | Viscosity at 1.2% | Loss on Drying |
|---|---|---|
| ACT591 | 39–91 mPa·s | ≤7.0% |
| ACT3212 | 50–200 mPa·s | ≤7.0% |
| ACT611 | 50–151 mPa·s | ≤7.0% |
| ACT538 | 39–175 mPa·s | ≤7.0% |
| ACT521 | 50–100 mPa·s | ≤7.0% |
Formulators should confirm grade selection through application testing in the target beverage matrix. The viscosity ranges above represent product specifications, and formulators should not interpret them as guaranteed beverage performance.
Need help matching a stabilizer to your protein beverage? To request a technical evaluation, send: protein source and content + total solids + fat/oil level + pH + mineral fortification level + current stabilizer and dosage + main stability problem + processing conditions (pasteurization/UHT) + monthly volume — and we can help identify suitable grades for laboratory screening.
Before changing the stabilizer, identify what is actually failing — the fix should match the mechanism, not just the symptom.Troubleshooting protein drink stabilizers should focus on the mechanism behind the instability rather than simply increasing stabilizer dosage.
| Observed Problem | First Variables to Check | Stabilizer Strategy to Evaluate |
|---|---|---|
| Bottom sediment | Protein type, particle size, dispersion | Colloidal MCC, CMC, or a combination |
| Sediment resists redispersion | Aggregation, particle structure | Suspension-system optimization, not higher dosage |
| Top cream layer | Fat/oil droplet size, homogenization | Emulsification + a compatible stabilizer system |
| Excessive thickness | Dosage, grade, total solids | Lower dosage or an alternative, lower-viscosity grade |
| Gritty or chalky mouthfeel | Protein particle size, hydration | Process optimization before assuming a stabilizer problem |
| Stable at bench scale, unstable after commercial processing | Heat treatment, homogenization, scale-up | Re-validate under the actual commercial process |
A useful troubleshooting sequence follows the same logic regardless of the specific defect: define the failure precisely, identify when it first appears (immediately after mixing, after homogenization, or only after storage), review the process step associated with that timing, then change one major variable at a time so cause and effect stay traceable. A formulation is not automatically “wrong” just because a defect appears — often the stabilizer is not the main problem, and protein quality, water quality or a process step deserves scrutiny first.
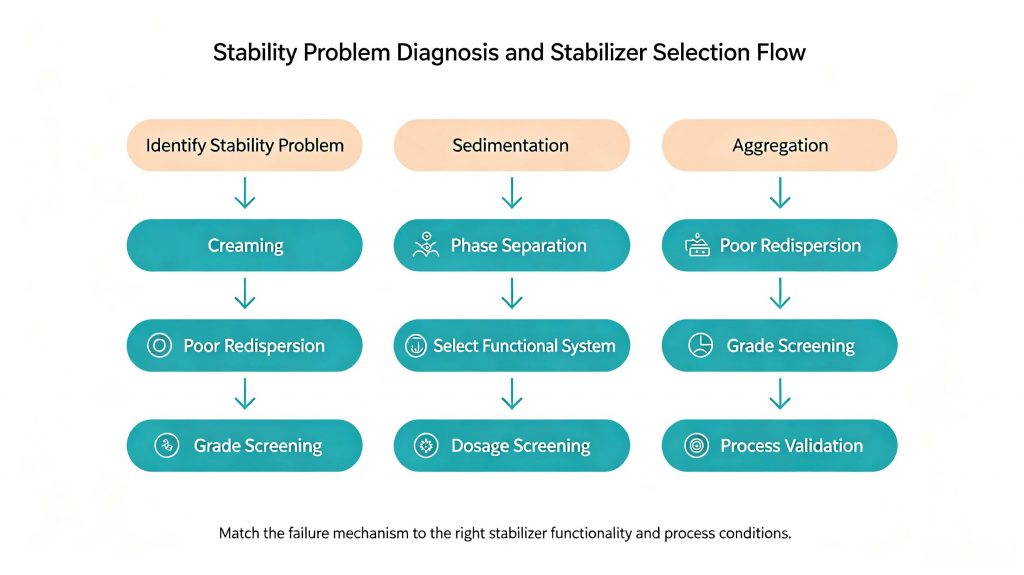
Many protein beverages require more than one functional mechanism at the same time. For example, formulators may need to control protein sedimentation while also managing body and emulsion stability in fat-containing systems. In these cases, formulators can assign each ingredient a specific role and use a combination system to achieve a better functional balance than a single ingredient at a high dosage, particularly when the formulation needs to address multiple stability requirements simultaneously.
| Combination | Functional Logic | What to Watch For |
|---|---|---|
| Colloidal MCC + CMC | Suspension structure + water-phase/viscosity support | No universal ratio — validate for each formulation and process |
| Colloidal MCC + Xanthan Gum | Suspension + controlled shear-thinning rheology | Total viscosity can rise faster than expected |
| CMC + Modified Starch | Water-phase control + body/texture | Modified starch is sensitive to heat and shear — test under the real process |
Avoid stacking stabilizers just because each one “sounds right” for part of the problem; combining several ingredients without a clear functional reason usually raises viscosity, cost and troubleshooting difficulty all at once, without necessarily improving stability. A simpler system with clearly defined roles is easier to control and easier to diagnose when something changes.
Building a robust system also means testing against realistic variation, not just a single best-case batch: different protein lots, minor pH shifts, and normal commercial-process variation should all be part of the evaluation before a formulation is considered finalized.
Dosage serves as an optimization variable, not a default fix. Using too little stabilizer can leave the beverage with sedimentation, weak body and poor stability, while using too much can create excessive viscosity, poor pourability, a gummy texture, higher cost and processing difficulties. Formulators should aim to identify the lowest practical dosage that consistently meets the required stability, sensory and processing targets. Controlled trials should establish this dosage rather than having formulators increase one ingredient until the visible problem disappears.
When optimizing protein drink stabilizers, formulators should evaluate grade selection before simply increasing dosage.
ACTA Technical Insight: Screen the Grade Before Optimizing the Dosage The same ingredient can behave very differently across viscosity grades: hydration behavior, processing behavior, finished-product viscosity and suspension response can all shift from grade to grade at an identical dosage. For this reason, ACTA recommends against fixing a dosage first and then searching for a grade that fits it. The more reliable sequence is grade screening → dosage screening → process validation — if a formulation only reaches the required stability at an unacceptably high viscosity, test a different grade before raising the dosage further.
Processing Is Part of the Formulation
| Process Step | What to Control |
|---|---|
| Powder addition and dispersion | Sequence, avoiding local over-concentration, mixing intensity |
| Hydration | Water temperature and hydration time |
| Homogenization | Pressure, number of passes, product temperature |
| Heat treatment | Pasteurization/UHT profile and its effect on protein and viscosity |
| Cooling and filling | Temperature control through to fill |
Addition order and hydration deserve particular attention in protein systems, because dispersing a stabilizer poorly — or adding it at the wrong point relative to the protein and minerals — can create local over-concentration that looks like an ingredient failure but is really a process issue. Homogenization and heat treatment should also be evaluated as part of the stabilizer system rather than as separate steps, since both can change how a given grade performs in the finished beverage.
A stabilizer strategy that works for one protein-beverage category will not automatically transfer to another, because protein source, total solids, pH and product format all change what “stable” requires.
| Application | Primary Consideration | Typical Starting Point |
|---|---|---|
| Whey protein RTD beverages | Heat-sensitive whey protein interactions | Colloidal MCC-based suspension, validated after UHT/pasteurization |
| Pea and soy protein beverages | Aggregation, grittiness and sedimentation tied to the protein source | Characterize the protein first, then screen suspension systems |
| Rice and mixed plant-protein beverages | Thin body combined with sedimentation | A body-building component paired with a suspension component |
| High-mineral-fortification beverages | Mineral-protein interactions changing formulation behavior | Compare fortified vs. non-fortified versions before finalizing dosage |
| Acidic (low-pH) protein drinks | Protein stability shifts with pH | Evaluate protein-compatible systems (e.g., suitable pectin or MCC-based systems) at finished-product pH |
| Clear or translucent protein drinks | Optical clarity is a primary formulation constraint | Prioritize protein solubility, particle-size control, filtration/clarity requirements and clarity-compatible stabilizer systems before evaluating suspension-oriented ingredients |
| Meal-replacement or high-total-solids beverages | Multiple mechanisms (protein, fat, fiber) failing at once | Diagnose suspension and emulsion issues separately before combining ingredients |
Two patterns are worth calling out because they trip up otherwise solid development programs. First, a formulation that is stable in the laboratory but not in commercial production usually points to a scale-up or process gap rather than a stabilizer failure — re-validate after the actual heat treatment and homogenization conditions, not just the bench trial. Second, different protein lots can produce different stability results at an identical stabilizer dosage, which means protein variability, not the stabilizer, is often the first thing worth investigating when a previously reliable formulation suddenly behaves differently.
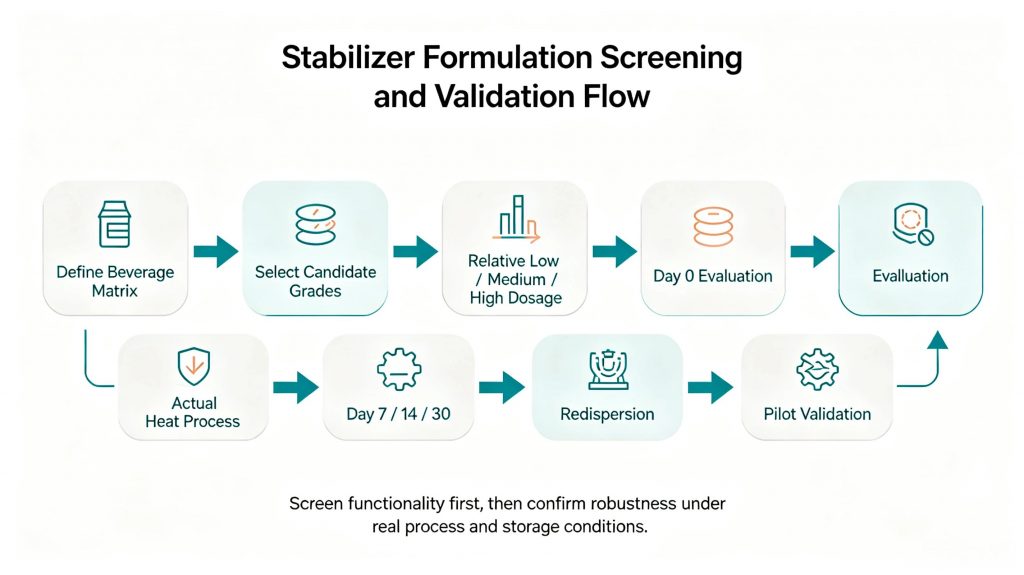
Passing an immediate post-processing check is not the same as demonstrating shelf-life stability. Track sedimentation, creaming, viscosity drift, redispersibility, sensory attributes and pH across the observation schedule introduced in Section 2, and record trends rather than a single pass/fail result — a viscosity that drifts slowly downward, or sediment that slowly increases, can signal a longer-term problem even when the current sample still looks acceptable.A protein drink stabilizer that performs well immediately after processing still needs to be evaluated during storage and under the actual commercial process.
Protein Beverage Stabilizer Screening Workflow
Scale-up deserves its own validation step rather than an assumption that a 2-liter bench result will hold at 2,000 liters. Pilot-scale verification should confirm that homogenization, heat treatment and mixing behave consistently at the larger scale, and a commercial batch should be compared against the original approved sample — not just against a specification range — before the formulation is considered locked in.
Define target ranges for viscosity, sedimentation, redispersion score, appearance, mouthfeel and pH before running the trial, as internal development targets specific to the product category rather than universal industry limits. Robustness testing — deliberately varying pH, protein lot or minor process parameters within a realistic range — shows whether the formulation has a genuine operating window or only works at one exact set of conditions, which matters directly once the product moves into routine commercial production with normal batch-to-batch variation.
Once a stabilizer system and grade look technically suitable, the question shifts from formulation to sourcing: can the supplier provide that exact grade consistently, with the documentation and commercial terms a production line needs? At minimum, confirm the exact grade (not just the ingredient name), request TDS, COA and SDS for that specific grade, clarify MOQ and lead time, calculate cost-in-use rather than price per kilogram, and check batch consistency and change-control practices before approving a supplier for commercial use.
Cost-in-use per ton of beverage = Σ (ingredient price per kg × ingredient dosage in kg per ton of beverage). Illustrative example: Supplier A quotes $4/kg at a 1.0% dosage → $40/ton of beverage; Supplier B quotes $7/kg at a 0.4% dosage → $28/ton of beverage. The higher-priced material is the lower cost-in-use once dosage is accounted for, so comparing suppliers on price per kilogram alone can produce the wrong decision.
| Information | Why It Matters |
|---|---|
| Protein source and content | Determines aggregation and interaction risk |
| Total solids and fat/oil level | Indicates suspension vs. emulsion requirements |
| pH and mineral fortification | Affects formulation compatibility |
| Current stabilizer and dosage | Provides a cost-in-use baseline |
| Main instability problem | Defines the technical target |
| Processing conditions (pasteurization/UHT) | Helps select a heat-appropriate grade |
| Monthly volume and destination market | Supports accurate commercial quotation |
| Supplier Capability | Why It Matters |
|---|---|
| Multiple grades | Allows formulation screening |
| Consistent viscosity | Reduces batch-to-batch variation |
| TDS/COA/SDS | Supports technical qualification |
| Application support | Reduces trial-and-error |
| Sample availability | Enables laboratory screening |
| Stable production capacity | Supports scale-up |
| Change-control process | Protects approved formulations |
| Export documentation | Supports international procurement |
| Batch traceability (batch number, production date, COA-to-batch consistency) | Supports change notification and specification consistency over time |
A supplier sample may perform well in laboratory trials, but manufacturers should confirm its performance through pilot and commercial production before they fully qualify the material. Buyers should also establish in advance which changes, such as manufacturing site, raw-material source or specification changes, require supplier notification and possible requalification.
For beverage manufacturers evaluating colloidal MCC, MCC Gel or CMC for protein drink stabilization, ACTA can serve as a potential supply partner for application-oriented evaluation. Each manufacturer should confirm the final grade and dosage through its own formulation and processing trials.
Selecting protein drink stabilizers for commercial production requires evaluation of technical performance, batch consistency, documentation, supply continuity and cost-in-use.Buyers evaluating long-term cellulose ingredient supply can also review our Global Cellulose Supplier guide.
For commercial protein beverage development, the regulatory status of each stabilizer should be checked for the target market and intended use. In the United States, manufacturers should verify the applicable regulatory status and conditions of use for food ingredients through the FDA food additives and GRAS resources rather than assuming that an ingredient is permitted simply because it is commonly used in beverages.
For products intended for the European market, regulatory review should also consider the applicable EU requirements for food additives, including their authorised uses and conditions of use. EFSA’s food additives resources provide scientific and regulatory background for evaluating food additive safety in the European Union.
For international formulation and export projects, Codex references can provide an additional point of reference when reviewing food additive functions, food categories and permitted conditions of use. The Codex General Standard for Food Additives (GSFA) provides a searchable database of adopted food additive provisions by additive, functional class and food category.
One-Page Development Logic
1. Beverage        → What protein source, format and target market?
2. Problem         → What is unstable, or what could fail?
3. Mechanism       → Sedimentation, aggregation, creaming, viscosity or redispersion?
4. Candidate       → Which stabilizer system should be screened?
5. Grade           → Which exact grade, screened before dosage?
6. Dosage          → At what practical, minimum-effective level?
7. Process         → How should it be dispersed, hydrated, homogenized, heated?
8. Stability       → Does it hold through Day 0/7/14/30/extended storage?
9. Scale-up        → Does the bench result hold at pilot and commercial scale?
10. Cost           → Is the cost-in-use commercially acceptable?
11. Supplier       → Can the exact grade be supplied consistently, with documentation?
Commercial Approval Checklist
There is no single best stabilizer — the right choice depends on the beverage’s dominant failure mode (sedimentation, aggregation, creaming or excessive viscosity) and on its protein source, total solids and processing conditions. Section 3 covers how to compare MCC, CMC, xanthan gum and modified starch for a specific protein system.
Sedimentation typically comes from protein or mineral-protein particles settling under gravity, sometimes accelerated by aggregation. Identifying what is actually settling — protein, mineral complexes or another insoluble component — should come before selecting a stabilizer.
CMC primarily supports viscosity, hydration and water-phase behavior. Depending on the formulation, it may help reduce settling by modifying the continuous phase, but it does not necessarily provide the same suspension structure as a colloidal MCC system.
Pasteurization and UHT can change protein conformation and protein-protein interactions, so a stabilizer system that performs well in an unheated bench sample does not automatically perform the same way after commercial heat treatment — always validate after the actual thermal process, not just the cold trial.
Formulators should determine the appropriate dosage based on the protein source, total solids, stabilizer grade and beverage matrix. They should establish the final dosage through controlled formulation trials rather than relying on a generic percentage.
Protein lots can vary in composition and processing history, which changes how they interact with a stabilizer even at an identical dosage — this is a common root cause when a previously reliable formulation suddenly becomes unstable.
Evaluate the sediment structure, not just its volume — a loose sediment that redisperses easily is a different problem from a compact, aggregated sediment that resists shaking. A suspension-oriented system such as colloidal MCC is typically evaluated for the latter case.
Confirm the exact grade (not just the ingredient name), request TDS/COA/SDS for that grade, run controlled lab trials, validate a pilot and commercial batch, and compare cost-in-use — not price per kilogram alone — alongside lead time, MOQ and change-control practices.
MCC Gel-type colloidal MCC systems primarily build a suspension structure that holds particles in place with limited added viscosity, while CMC mainly contributes viscosity, hydration support and water-phase stability — the two are often complementary rather than substitutes.
Formulators can evaluate colloidal MCC in high-protein beverages when particle and protein suspension represents the primary concern, particularly when the formulation needs to maintain suspension without making the beverage too thick to drink. Formulators should still confirm the appropriate grade and dosage through application testing in the specific beverage matrix.
Start by screening several candidate grades under the same conditions before optimizing dosage — viscosity, hydration behavior and processing performance can differ meaningfully between grades of the same ingredient, as covered in Section 6.
Yes. Colloidal MCC and CMC can be evaluated together when the formulation needs both suspension structure and water-phase viscosity/hydration support. The ratio should be validated for each formulation.
Protein source and content, total solids, fat/oil level, pH, mineral fortification, current stabilizer and dosage, the main stability problem, and processing conditions (pasteurization/UHT) — this lets a supplier recommend relevant grades for screening.
The right protein drink stabilizer strategy starts with the beverage, not the ingredient: define the protein system, identify the actual instability, understand its mechanism, select a functional system and exact grade, optimize dosage and processing together, validate stability through storage and scale-up, calculate cost-in-use, and qualify the supplier through specifications and consistent supply. This applies across whey, pea, soy, rice and mixed-protein beverages alike — the goal is not the single strongest stabilizer, but the right system, at the right grade and dosage, that a supplier can deliver consistently for commercial production.
Send us these 10 points and we can help identify suitable grades for laboratory screening and prepare a commercial quotation where appropriate:
Plus, for commercial quotation: monthly volume, destination market, packaging requirement.
