Author: Richard Wang | Technical Review: Alice Meng | Company: Qingdao ACTA Biotechnology Co., Ltd about low viscosity CMC
Low viscosity CMC is a carboxymethyl cellulose grade that delivers a relatively low solution viscosity under defined test conditions. Buyers choose it when they need water-soluble functionality without excessive thickening. However, picking the right grade takes more than choosing the lowest viscosity number. This guide explains the properties, specifications, applications, troubleshooting methods, quality controls, and purchasing steps that help you select a dependable low viscosity CMC supplier and request an accurate quotation.
Need help selecting a low viscosity CMC grade? Tell ACTA how you plan to use the product, what performance you need, and whether you have an existing specification or reference sample. If your target viscosity or test method is not yet defined, share the application details first. ACTA can review the information and confirm which sodium CMC product options, technical documents, and commercial terms may suit your requirements, or you can use the quotation form.
Caption:Low viscosity sodium CMC is selected according to the required viscosity, formulation, and application performance.
Low viscosity CMC is a grade of sodium carboxymethyl cellulose designed to provide relatively low solution viscosity under specified test conditions. Depending on the formulation, it may contribute to water retention, binding, texture modification, or liquid-phase control without producing the same level of thickening as a higher-viscosity grade.
However, low viscosity does not automatically mean better performance. The appropriate grade depends on the intended function, formulation, processing conditions, and required product characteristics.
When selecting a grade, consider both its measured viscosity and its performance in the complete formulation. A product that works well in one application may not provide the same results in another.
In most commercial contexts, the two terms describe the same category. Even so, you should confirm chemical identity and grade rather than trust a product name alone. Sodium CMC is the sodium salt of carboxymethyl cellulose, and suppliers offer it in many grades that differ in viscosity, purity, degree of substitution, moisture, particle characteristics, and application suitability.
These differences matter. Two products with similar viscosity readings can perform differently in a finished formulation. Moreover, “low viscosity” describes a performance trait, not purity, regulatory status, or food or pharmaceutical suitability. Always review the technical data sheet (TDS), certificate of analysis (COA), and compliance documents before approving a grade.
Manufacturers select low viscosity CMC when they want some CMC functionality while keeping handling manageable. The main reasons include:
However, these benefits are not guaranteed. Actual results depend on dosage, equipment, and the full recipe. Therefore, validate any grade change through laboratory trials and production-scale confirmation. The best grade is the one that meets technical requirements reliably and economically, not necessarily the cheapest or the thinnest.
Low viscosity CMC is worth evaluating when a formulation needs sodium CMC functionality without excessive thickening. Before selecting a grade, define the required viscosity under an agreed test method, identify the main function, and check compatibility with the complete formulation. If particle suspension is the primary objective, evaluate whether CMC alone is sufficient or whether another stabilizer system is required.
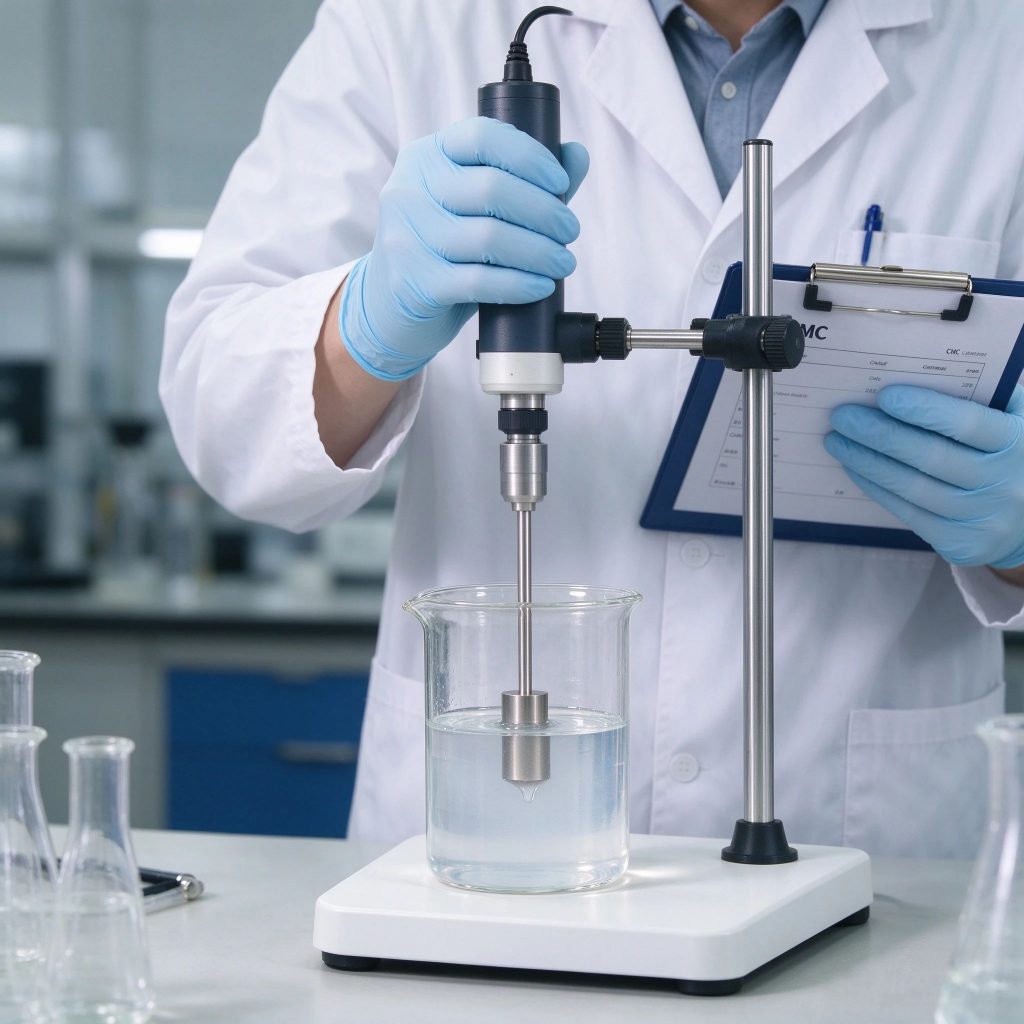
Caption:CMC viscosity results should be compared using consistent concentration, temperature, and measurement conditions.
Viscosity is usually the first specification buyers check, yet a number means little without its method. Suppliers report viscosity in mPa·s or cP, and these units are numerically equivalent (1 mPa·s = 1 cP). Still, matching units do not make products comparable.
Consider two hypothetical grades. Grade A reports 80 mPa·s at 1% and 25°C. Grade B reports 150 mPa·s at 2% and 25°C. Because the concentrations differ, you cannot tell which product is thinner under equivalent conditions. Concentration, temperature, instrument, spindle, rotational speed, hydration time, and mixing procedure all influence the result.
Buyer tip: State the target range, concentration, temperature, and method in your inquiry. If you lack a method, ask the supplier for its standard procedure and a representative COA.
A viscosity value is directly comparable only when the test conditions are sufficiently consistent. At a minimum, agree the concentration, temperature, instrument and spindle, speed or shear conditions, hydration time, sample preparation, and units with the supplier.
ACTA’s published viscosity information: ACTA lists sodium CMC with low, medium, and high viscosity grades on its CMC product page. However, a product-range figure does not define the viscosity of any single low viscosity grade, so select the grade according to the required viscosity, concentration, temperature, and test method. Confirm the specific grade and its applicable viscosity specification in the current TDS and batch COA before ordering, and ask ACTA whether a customized viscosity or DS grade suits your application.
Degree of substitution (DS) is the average number of hydroxyl groups replaced by carboxymethyl groups per anhydroglucose unit. It influences solubility, solution uniformity, compatibility with other ingredients, and performance in salt-containing systems.
Nevertheless, DS cannot predict viscosity by itself. Two grades with similar DS can differ in viscosity because chain length, molecular-weight distribution, and manufacturing conditions differ. Likewise, a higher DS is not automatically better. If your process requires a defined DS range, write it into the inquiry and request supporting documentation. If molecular weight matters, ask whether the supplier actually measures it; a verified viscosity specification plus a successful application trial often proves more useful than an estimated molecular weight.
DS in ACTA’s published specifications: ACTA’s published food-grade (E466) specification lists a DS of 0.65–1.20, and its pharma-grade specification lists 0.65–0.95. Confirm the applicable range for your selected low viscosity grade in its current TDS and the agreed purchasing specification. Grade guidance for protein beverages, plant-based milk, and acidic drinks depends on protein type, pH, mineral content, heat treatment, and the overall stabilizer system, so a DS value alone cannot guarantee stability. Evaluate the target grade in the complete formulation and confirm performance under the intended processing conditions.
DS is one grade-selection parameter, not a standalone predictor of viscosity or finished-product stability. Combine it with the viscosity specification, the other formulation ingredients, and application testing.
Purity requirements vary by application. Therefore, clarify what a supplier means by purity: an assay, sodium CMC content, or another measurement, together with the method and calculation basis. A high purity figure does not prove food or pharmaceutical grade; documentation must support that claim.
Moisture deserves equal attention. Two materials with different moisture contents deliver different amounts of dry CMC per kilogram. Moisture can also affect caking and storage stability under poor conditions. Compare the maximum moisture limit, the analytical method, the reporting basis, the batch COA value, and the recommended storage conditions.
Published general specifications for ACTA food-grade and pharma-grade CMC. The table below summarizes the typical parameters ACTA publishes for its two main grades. They are general specifications for the listed grades, not specifications of one low viscosity grade, so treat them as reference ranges that can differ by grade and intended use; the term “pharma grade” alone does not establish compliance; the current TDS, the test method stated on it, and the batch COA for your grade govern each order.
CMC specifications vary by grade, manufacturer, application, and regulatory requirements. The following table is a general purchasing reference, not a universal specification for all low-viscosity CMC products.
Low viscosity describes performance under defined test conditions; it does not automatically establish food-grade status, pharmaceutical suitability, or regulatory compliance.
| Parameter | Food Grade (E466) | Pharma Grade (as listed by ACTA) |
|---|---|---|
| Appearance | White to off-white powder | White to off-white powder |
| Degree of substitution | 0.65–1.20 | 0.65–0.95 |
| Assay (dry basis) | ≥ 99.5% Na-CMC | ≥ 99.5% Na-CMC |
| Moisture content | ≤ 10% | ≤ 10% |
| Heavy metals (as Pb) | ≤ 10 ppm | ≤ 10 ppm |
| NaCl content | ≤ 0.5% | ≤ 0.2% |
| pH (1% solution) | 6.5–8.5 | 6.5–8.0 |
| Particle size (d90) | Customizable | As specified |
Note: Actual limits depend on the selected grade, its current specification, and applicable requirements. Verify these values with the supplier before purchasing.
Request the current Technical Data Sheet (TDS), agreed product specifications, and batch-specific Certificate of Analysis (COA). Confirm the viscosity range, solution concentration, test temperature, measurement method, and acceptance limits.
ACTA’s quality system page describes inspection items including viscosity, particle size, moisture, pH, ash, microbiology, and heavy metals. Confirm which tests apply to your selected grade and are included in its documentation.
Pharmaceutical suitability must be verified against the applicable pharmacopoeial monograph, test methods, impurity limits, market requirements, and intended use. A general grade description or specification table alone does not establish pharmaceutical compliance.
Choose a grade according to your application, required viscosity under defined test conditions, quality requirements, and applicable regulations. Confirm the product’s compliance status and acceptance criteria with the supplier before use.
Caption:Buyers should review the agreed product specifications, test methods, and batch documentation when qualifying a CMC supplier.
Critical requirements vs. performance preferences. Separate the two before you send an inquiry, because they change how a supplier screens grades.
| Category | What it means | Examples |
|---|---|---|
| Critical requirements | Not met, do not purchase | A mandatory viscosity range under the agreed test method, regulatory requirements for your target market, customer-specified purity or impurity limits, required documents |
| Performance preferences | Can be optimized in trials | Ease of dispersion, processing convenience, effective dosage, texture, handling |
The example below illustrates a comparison method. It is not ACTA product data.
| Comparison item | Supplier A | Supplier B | How the buyer should judge |
|---|---|---|---|
| Test concentration | 1% | 2% | Check whether the concentration is the same |
| Test temperature | 25°C | 25°C | Confirm the temperature matches |
| Test method | Method A | Method B | Request the full method and instrument conditions |
| DS | To be provided | To be provided | Check against the purchasing requirement |
| Moisture | To be provided | To be provided | Compare with the agreed specification |
| Batch COA | To be provided | To be provided | Verify the results for the specific batch |
| Formulation result | Not yet completed | Not yet completed | Run a control test in the same formulation |
You cannot rank these two grades by their reported viscosity values alone, because the test concentrations and methods differ. Request comparable viscosity data from both suppliers, then evaluate both products in your intended formulation.
Do not convert a 1% result to a 2% result yourself, and do not infer which product is better without experimental evidence.
Use the following sequence to move from an application requirement to an approved CMC grade.
Step 1: Define the function.
Identify whether you need limited thickening, water retention, binding, flow control, or another specific function. Define the performance problem that the ingredient must solve.
Step 2: Set the viscosity specification.
Specify the target viscosity range, solution concentration, test temperature, measurement method, and relevant instrument settings. If you do not have a fixed target, provide the reference product or describe the required performance.
Step 3: Confirm grade requirements.
Review the required degree of substitution (DS), moisture, purity, impurity limits, particle characteristics, and application-specific compliance requirements. Not every parameter has the same importance for every application.
Step 4: Verify the documentation.
Request the current TDS and relevant compliance documents. Review a representative COA during supplier evaluation and confirm the batch-specific COA requirements for commercial orders.
Step 5: Test the complete formulation.
Evaluate candidate grades under consistent preparation, mixing, processing, and measurement conditions. Assess the actual application performance rather than relying on viscosity values alone.
Step 6: Approve the purchasing specification.
Before commercial purchasing, document the approved grade, agreed specification, test method, critical acceptance limits, packaging requirements, documentation requirements, and change-control expectations.
This process helps buyers distinguish between a grade that appears suitable on paper and one that has been validated for the intended application.
When evaluating food-grade sodium carboxymethyl cellulose, buyers can consult the FAO JECFA specifications for sodium carboxymethyl cellulose as a reference for applicable food additive specifications. Commercial grades may have additional viscosity and application-specific requirements, so buyers should also review the supplier’s technical data sheet (TDS), certificate of analysis (COA), and agreed product specifications.
Particle size affects handling, dispersion, hydration, and lump risk. Finer powder does not guarantee better performance, because poor addition practices still cause lumps. Evaluate particle data together with your preparation method, and run a practical dispersion test when appearance or processing consistency matters.
Similarly, compare pH only when concentration and preparation match. Other parameters may apply depending on use: ash, residual salts, heavy metals, microbiological limits, and batch identification. Separate mandatory acceptance criteria from informational requests so that procurement stays efficient while critical quality attributes remain controlled.
Technical Documents and Certification Verification
Before qualifying a CMC supplier, confirm which documents are available for the selected product and manufacturing site.
Certification claims should be checked against the current document, including the certificate holder, manufacturing site, scope, validity period, and applicable product categories. A management-system certificate does not automatically mean that every product manufactured by the company has a separate product certification.
Before publication or purchase, confirm the exact certification name and current status. Do not describe a certificate, a certification statement, and a technical document as equivalent forms of certification.epend on the selected grade, application, and destination-market requirements, so confirm document availability and scope before ordering, and request the batch-specific COA with each shipment.
Before you approve a low viscosity CMC grade, separate mandatory requirements from performance preferences.
Base a supplier qualification decision on documented requirements, comparable test results, and application performance, not on a product name or a single viscosity figure.
In food manufacturing, sodium CMC can act as a thickener, stabilizer, water-retention agent, or texture modifier. Low viscosity grades suit products that must stay relatively fluid, including beverages, sauces, dressings, bakery items, and other aqueous systems.
Low viscosity CMC may serve different functions in food and beverage formulations, including water retention, texture modification, binding, and viscosity control. Its contribution depends on the product matrix, processing conditions, dosage, and interactions with other ingredients.
In beverage applications, the required performance should be defined before selecting a grade. A formulation may require limited thickening, improved mouthfeel, reduced separation, or a combination of these functions. These outcomes are not interchangeable, and they should be evaluated separately during formulation trials.
Selecting CMC viscosity grades for beverage applications: Selecting a CMC grade for a beverage requires more than choosing a low viscosity value. Buyers should consider the beverage’s composition, pH, soluble solids, processing conditions, storage requirements, and the desired final texture.
For beverages containing suspended particles, viscosity alone may not provide sufficient stability. The formulation may require a different stabilization strategy, including an appropriate hydrocolloid system or a combination of ingredients. The suitability of each approach must be verified in the intended formulation.
Where sedimentation control is the main goal, compare CMC with other stabilizer systems such as colloidal MCC. See ACTA’s beverage stabilizer solutions for more.
Cellulose derivatives appear in pharmaceutical formulations, yet suitability depends on the specific material, dosage form, and quality requirements. A material that satisfies an industrial viscosity specification is not automatically suitable for pharmaceutical use.
Purchasers should confirm the applicable pharmacopoeial or customer specification, identification, viscosity under prescribed conditions, impurity controls, batch consistency, traceability, and change-control procedures. Furthermore, avoid describing low viscosity CMC as a universal tablet binder, disintegrant, or coating agent; define the intended function and verify the supplier’s documentation first.
Detergent makers may evaluate CMC for soil suspension, textile processors for printing and sizing, and paper and coating producers for water-based rheology and binding. In each case, test compatibility, dosage, storage stability, and batch consistency under actual operating conditions, because laboratory viscosity alone rarely predicts process performance.
Grade labels are relative and vary between suppliers.
| Factor | Low viscosity | Medium viscosity | High viscosity |
|---|---|---|---|
| Solution viscosity | Relatively low | Intermediate | Relatively high |
| Typical objective | Limited thickening | Balance of flow and body | Strong thickening |
| Processing | May ease flow in some systems | Needs flow and texture checks | May need closer mixing control |
| Main criterion | Function at acceptable viscosity | Functionality and processability | Thickening and process fit |
These categories are relative descriptions, not universal viscosity ranges. Actual classification depends on the supplier’s grade definitions and the specified test method. Always compare products using equivalent test conditions.
Choose low viscosity when the product must stay pourable, when handling limits matter, or when you need controlled rather than maximum thickening. Choose a higher grade when a lower one cannot deliver the function at a practical dosage. Still, reducing viscosity without finding the cause of instability may make a product flow better but separate faster. Replacement never rests on labels alone: compare complete specifications, run a controlled trial against your current grade, test alternative dosages, and confirm at production scale.
Low viscosity CMC is not inherently more stable than other grades, and it does not by itself solve sedimentation. See the troubleshooting guidance in Part 4, and evaluate other stabilizer systems where suspension is the main goal.
For applications in the United States, manufacturers should verify the regulatory requirements applicable to the intended food use. The U.S. FDA regulation for sodium carboxymethylcellulose, 21 CFR § 182.1745 provides a regulatory reference for this substance. Compliance should be assessed according to the applicable conditions of use and the requirements for the finished product.
Xanthan gum is a microbial polysaccharide with pronounced shear-thinning behavior. Guar gum is a plant-derived galactomannan. Sodium CMC is a modified cellulose. Because their structures differ, their hydration, rheology, and compatibility differ as well.
Consider CMC when you need its specific functionality with limited viscosity contribution. Consider xanthan when its distinctive rheology matters, and guar when its thickening profile fits. Neither is universally superior. Compare candidates at practical dosages in the same formulation, and calculate cost at the dose that achieves the target rather than price per kilogram.
CMC is anionic, whereas HPMC and HEC are nonionic cellulose ethers; this difference changes behavior in the presence of salts, proteins, and surfactants. Standard MCC is insoluble and works mainly as a bulking agent, texturizer, or excipient. Colloidal MCC is a specialized dispersion system, usually formulated with a stabilizing component such as sodium CMC, and it provides stabilization that ordinary low viscosity CMC alone does not.
Therefore, treat these materials as different tools rather than interchangeable ones. Even similar viscosity readings can hide different behavior in the actual product. Support any switch with comparative testing, and compare specific grades, not categories.
For grade-level specifications of these alternatives, review ACTA’s HPMC, microcrystalline cellulose, and colloidal MCC pages.
Caption:Proper powder dispersion and hydration help improve preparation consistency. Suitable processing conditions depend on the CMC grade and formulation.
Start with the problem, not the product. Follow five steps: identify the primary function; define finished-product requirements; review compatibility with pH, salts, proteins, and other hydrocolloids; compare options at practical dosages; and confirm quality and documentation needs.
When you replace an ingredient, establish a baseline first, define the objective (cost, processing, texture, supply, or specification), change one major variable at a time, and evaluate performance beyond initial viscosity, including storage behavior. Finally, document the approved specification before commercial purchasing, and route material changes through your change-control system.
When CMC performance differs from expectations, investigate the material, preparation process, formulation, and measurement conditions before changing the dosage.
Use the following sequence:
This sequence helps identify the likely cause before making unnecessary formulation changes or replacing the ingredient.
Hydration and dissolution differ. It is the polymer’s interaction with water; dissolution is the formation of a uniform solution. A powder can look wet outside while staying dry inside, which creates slow-hydrating lumps. Powder addition rate, mixing intensity, temperature, concentration, and other ingredients all matter.
Water quality also counts. Dissolved salts, hardness, and pH can change how a charged polymer behaves, so a grade that performs in deionized water may act differently in process water. Likewise, proteins and other hydrocolloids can interact with CMC. Test in representative water and in the complete formulation, change one factor at a time, and record pH, ingredient sequence, and conditions.
CMC performance in acidic beverages depends on the grade, pH, ionic composition, and other formulation ingredients. Under strongly acidic conditions, changes in solubility, viscosity, or compatibility may occur. A higher degree of substitution may be worth evaluating in some formulations, but it does not guarantee stability in every system. Test the selected grade in the complete beverage formulation and assess performance after the intended heat treatment and during storage. Where additional suspension support is needed, compare CMC with an appropriate stabilizer system, including colloidal MCC where technically suitable. Divalent ions such as calcium may also affect CMC viscosity and compatibility, depending on their concentration, the selected grade, and the overall formulation. For calcium-fortified or dairy-based beverages, evaluate the ingredient system under the intended processing conditions rather than relying on viscosity measured in water alone.
No universal dosage exists. The correct level depends on function, ingredients, processing, and target performance. Establish a control formulation, test candidate concentrations under identical conditions, and define acceptance criteria before the trial begins.
Because a viscosity result in water does not fully predict finished-product behavior, test the sample in the real formulation. Evaluate viscosity, appearance, sedimentation, texture, processability, and storage stability. Repeat critical measurements to confirm reproducibility, then document the decision.
There is no universal dosage for low viscosity CMC. ACTA’s product page cites 0.1–1.0% as a use-level window for CMC in general, so treat it only as a screening reference. Set the initial trial range from the selected grade, intended function, formulation, and supplier guidance, then optimize it through controlled application testing before you scale up.
Plant-based beverages contain proteins, fats, and suspended solids, so their stability demands differ from clear drinks. Evaluate CMC within the full system, including ingredient addition sequence and the effect of heat treatment or homogenization.
Do not judge stability by appearance alone. Measure viscosity and pH, track sediment over defined intervals, inspect what is separating (particles, aggregates, or an oil phase), and run storage studies at relevant temperatures. Because increasing viscosity may reduce particle movement yet harm texture or processing, aim for balance between suspension stability, flow, mouthfeel, and manufacturability.
Evaluate formulation cost per finished unit rather than price per kilogram; Part 6 shows the calculation. The mistakes below most often undermine a grade change.
Avoid these frequent mistakes:
When a CMC formulation underperforms, start with the root cause instead of changing grade or dosage. Sort possible causes into three groups: material-related (identity, batch, specification compliance), process-related (addition rate, mixing, hydration time, temperature), and formulation-related (pH, salts, proteins, other hydrocolloids). Record the batch number, quantity, preparation procedure, and observed result, and compare against an approved reference sample whenever possible.
| Problem category | Typical checks |
|---|---|
| Material | Product identity, batch, COA, and compliance with the agreed specification |
| Process | Addition rate, mixing method, hydration time, and temperature |
| Formulation | pH, salts, proteins, other hydrocolloids, and total solids |
Map each symptom below, such as lumps, low or high viscosity, sedimentation, and storage drift, to one of these categories before you change the grade or dosage.
Lumps and fish eyes may form when the outer surface of CMC particles hydrates before the powder disperses properly. The resulting hydrated layer can slow water penetration into the particle core.
To investigate the problem, review the order of addition, powder feeding rate, mixing conditions, hydration time, and water quality. Evaluate whether the existing process provides sufficient dispersion before extensive hydration occurs.
Do not assume that every hydration problem requires a different CMC grade. First establish whether the material and preparation process are consistent with the supplier’s instructions. Any process adjustment should be verified through controlled trials.
If viscosity falls below target, first verify concentration, weighing accuracy, hydration time, temperature, and instrument settings. Then compare the batch with a reference sample under identical conditions. Finally, review whether salts, acids, or other ingredients lower viscosity in the finished system. Do not raise the dosage to hide a possible nonconformity.
If viscosity runs high, check the powder-to-water ratio, measurement temperature, and recent formulation changes such as total solids or pH. Avoid uncontrolled dilution, because adding water changes solids, flavor, and yield. If the result stays out of specification after you verify the method, document it and contact the supplier with the COA, batch number, and test records.
Sedimentation is not determined by viscosity alone. Particle size, density, aggregation, ionic conditions, and processing all contribute. Identify what is separating before you change the grade. Particle settling, oil separation, and protein aggregation need different corrections.
For viscosity drift, confirm that initial hydration was complete, standardize measurement temperature, and check for evaporation, pH changes, and microbial growth in aqueous systems. Importantly, a dry powder’s shelf life does not guarantee that a prepared solution stays stable indefinitely; establish the holding time for your own formulation.
A formulation that works in a laboratory beaker may fail in a production tank because vessel geometry, impeller type, circulation, and addition equipment differ. Reproduce the key dispersion conditions rather than copying mixing time, and measure preparation time, agglomerates, and viscosity.
For scale-up or supplier substitution, evaluate CMC performance under conditions representative of the intended manufacturing process. Compare the relevant product specifications, processing behavior, and application results using consistent evaluation criteria. Before approving a new grade or supplier, conduct appropriate laboratory trials and, where necessary, pilot-scale or production validation. Acceptance should be based on documented performance against the application’s critical requirements rather than on nominal viscosity or purchase price alone.
Follow one general flow, then use the specific sections above for each symptom. First, verify product identity and batch documents. Second, check sampling, preparation, and test conditions. Third, review formulation and process variables. Fourth, compare against an approved reference sample. Fifth, record the results and contact the supplier if the problem remains unresolved.
When you contact a supplier, send facts instead of “it does not work.” Include the product grade, batch number, COA, application, preparation procedure, test concentration and temperature, instrument settings, observed defect, reference results, photographs, and corrective actions already tried. Keep measured facts separate from assumptions.
Batch consistency is an important consideration when qualifying a CMC supplier. Buyers should define the critical product characteristics that affect their application and agree on the relevant acceptance criteria before commercial supply.
Depending on the grade and application, these characteristics may include viscosity under specified test conditions, degree of substitution (DS), moisture, purity, pH, particle characteristics, or other agreed parameters. Not every parameter is necessarily tested or reported for every grade or batch.
A reliable quality-control process should define the applicable test methods, acceptance limits, batch identification, documentation requirements, and procedures for handling nonconforming results.
Upon receipt, verify the product name, grade, lot number, packaging condition, labeling, and required documents. Check that the supplied material matches the approved purchasing specification.
If incoming testing is required, use the agreed sampling procedure and test method. Viscosity results should be compared under equivalent conditions, including concentration, temperature, sample preparation, and measurement method.
Any difference between the supplier’s COA and the buyer’s test results should be investigated before the material is rejected or accepted. Differences in methods or preparation conditions may affect comparability.
When a batch does not meet an agreed acceptance criterion, document the lot number, test method, observed result, and relevant production or application conditions.
The supplier and buyer should investigate the discrepancy, identify the likely cause, and agree on appropriate corrective and preventive actions (CAPA), where applicable. The disposition of the affected batch should follow the agreed quality procedure.
Changes to the approved grade, manufacturing site, specification, or other critical supply conditions should be managed according to the parties’ change-control requirements. Where a replacement grade is proposed, verify its performance before treating it as interchangeable with the approved material.
Store CMC powder in its original, closed packaging in a clean, dry area away from water, condensation, strong odors, and chemicals. Keep bags off wet floors and away from leaks. Moisture can cause caking and dispersion problems, so inspect bags, liners, and pallet wrap on arrival.
Because no single shelf life fits every grade, confirm the declared shelf life or retest period in writing, and clarify whether the printed date means manufacturing, expiry, or retest. Follow the supplier’s temperature and humidity instructions instead of inventing limits. Manage stock with FIFO or FEFO, keep batch-level records, and do not extend shelf life based on appearance alone.
Storage recommendations for ACTA CMC: Store CMC in its original, sealed packaging in a clean, dry area protected from moisture, condensation, and contamination. Before you place an order, confirm the applicable shelf life, storage conditions, and retest requirements in the current technical documentation for your grade, and follow the instructions provided for that specific grade and batch.
Agree packaging before you confirm the order. Ask about net weight per bag, inner liners, outer packaging, palletization, labels, batch marking, and destination restrictions. Confirm custom labels or special liners in writing.
During transport, protect cargo from rain, crushing, punctures, and contamination, and inspect the container before loading. On arrival, document damage immediately. If bags arrive wet or torn, isolate them, photograph the condition, record the batch number, notify the supplier and carrier, request a quality assessment, and make a documented disposition decision. Wet or contaminated powder is not automatically recoverable.
ACTA packaging and shipping: ACTA’s listings mention 25 kg bags (plastic woven bags) or other formats according to customer requirements, and its site describes packaging customization and container loading coordination. Confirm the bag type, liners, palletization, labeling, and shipping port for your grade and destination in writing before dispatch.
Food grade and industrial grade are not interchangeable, even when viscosity and appearance match. Verify that the product satisfies the requirements of your intended use and destination market, and ask for evidence rather than a general claim.
Request the TDS, batch COA, and SDS, plus any product-specific compliance documents your market requires. Check that product names, grades, and batch numbers agree across labels, COA, and shipping papers. For export, confirm the commercial invoice, packing list, and certificate of origin where required. Never assume a supplier holds a certification until it provides proof.
Documents and certifications: Request the current TDS and batch-specific COA, the SDS and handling information, product-specific food-grade documentation where applicable, relevant certificates and declarations, and destination-market compliance information. ACTA lists ISO 9001, ISO 22000, ISO 14001, BRC, Halal, and Kosher certificates on its certificates page and can provide applicable product and compliance documentation for review. E466 is the food additive number for CMC, not a certification. Before qualification, confirm the validity, scope, covered products and sites, and issuing body of each required certificate, together with the regulatory status for your market and intended use.
| Information | Why it matters |
|---|---|
| Application | Helps identify the required function and suitability requirements |
| Target viscosity and test conditions | Makes technical data more comparable |
| DS and other critical limits | Defines the required technical acceptance criteria |
| Estimated quantity | Supports MOQ and quotation planning |
| Destination country or port | Helps determine shipping options and applicable commercial terms |
| Required documents | Clarifies product qualification and compliance needs |
| Reference product or specification | Helps assess potentially suitable alternatives |
You do not need to provide every technical detail at the first contact. Start with the application, target viscosity if known, estimated quantity, and destination. Additional technical requirements can be confirmed during the qualification process.
Minimum order quantity depends on the supplier’s policy, stock, grade, and packaging, so confirm sample, trial, and commercial MOQs separately. Use samples to test suitability, then move to commercial volumes after you approve the grade, acceptance criteria, and packaging.
A complete RFQ states the application, the target viscosity with its test concentration, temperature, and method, other specifications, required documents, quantity, packaging, destination, Incoterm, and sample needs. The template in Part 8 shows the wording.
By contrast, a request that says only “low viscosity CMC, price per kg” invites unsuitable quotations. If your specification is incomplete, describe the application and target performance, and mark unknown fields “to be confirmed.”
ACTA MOQ and samples: ACTA states that its MOQ depends on the product and grade, and that samples are available for evaluation. Its marketplace listings show a starting MOQ of 500 kg for CMC, but sample terms (including cost and shipping) and the applicable MOQ vary by grade and destination, so confirm them with ACTA. Include the product name, application, quantity, and target market in your inquiry.
The quoted price is only one part of total landed cost. Add packaging, inland transport, export handling, international freight, insurance, port charges, duties, taxes, customs clearance, and local delivery, as applicable to your agreed terms.
To compare cost properly, use this formula: CMC cost per metric ton of finished product = CMC price per metric ton × dosage percentage ÷ 100. Enter the dosage as a percentage figure, so 0.20% becomes 0.20, not 0.002. For example, a grade priced at USD 2,000 per metric ton and dosed at 0.20% costs USD 4.00 per metric ton of finished product, while a grade priced at USD 1,700 per metric ton and dosed at 0.25% costs USD 4.25. These figures are illustrative, not ACTA prices. In practice, add processing time, rejection risk, and batch stability to the comparison.
Before you switch to a lower-priced CMC grade, compare the dosage needed to reach the same functional result. A meaningful cost comparison should also weigh processing time, batch consistency, rejection risk, and the performance of the finished formulation.
The price of low viscosity CMC depends on the selected grade, required specifications, order quantity, packaging, documentation requirements, and delivery terms.
However, purchase price alone does not determine the overall cost of use. Buyers should also consider the dosage required to achieve the target performance, preparation efficiency, batch consistency, rejected material risk, and any additional processing costs.
When comparing quotations, confirm that the products meet equivalent technical requirements and that the quoted commercial terms cover the same scope. A lower price is meaningful only when the product is suitable for the intended application and the purchasing requirements are clearly defined.
Under FOB, the seller delivers goods on board the vessel you nominate at the named port. Under CIF, the seller arranges and pays cost, insurance, and freight to the destination port, although risk generally transfers at loading. Compare offers only on equivalent terms. Furthermore, separate production time, dispatch date, transit time, customs clearance, and final delivery when you plan a schedule, and allow time for incoming inspection.
Name the Incoterms version (for example, Incoterms 2020) and the named port in every quotation, and confirm exactly which costs and risks each party carries.
ACTA commercial terms: MOQ, sample arrangements, lead time, payment terms, packaging, and shipping options depend on the selected CMC grade, order quantity, destination, and current supply arrangements. Contact ACTA with your product requirements and estimated quantity to confirm the applicable terms, including when the lead time starts, before you place an order.
Demand for low viscosity CMC follows formulation-specific performance, process efficiency, batch consistency, and purchasing efficiency. Rather than rely on unverified market forecasts, evaluate verifiable supplier information: technical suitability, documentation, sample results, consistency, supply capability, packaging, commercial clarity, and technical communication.
To protect supply continuity, qualify an alternative supplier before a disruption, while recognizing that it is not automatically interchangeable. Estimate consumption, separate production, dispatch, and transit lead times, set a reasonable safety stock, and review supplier performance regularly. If sustainability matters, request documented evidence instead of inferring environmental benefits from product identity or packaging.
Use the scorecard below as an internal screening tool for comparing low viscosity CMC suppliers. The weights are illustrative, not an industry standard or validated best practice.
| Evaluation criterion | Suggested weight | What to assess |
|---|---|---|
| Technical suitability | 30% | Compliance with the agreed specification and performance in application trials |
| Documentation and compliance | 20% | Accuracy and availability of required technical and compliance documents |
| Batch consistency | 15% | Evidence of consistent results under agreed test conditions |
| Total cost | 15% | Product price, packaging, logistics, and relevant costs of use |
| Supply capability | 10% | Ability to support the expected order volume and delivery requirements |
| Communication and technical support | 10% | Clarity of responses, problem-solving, and change communication |
| Total | 100% |
Use the weights as an internal purchasing framework rather than a universal industry standard. Buyers can adjust them according to the application, quality requirements, and supply risks.
Treat technical specifications and regulatory requirements as pass or fail gates before you score. A supplier that fails a critical acceptance requirement should not be approved solely because of a high overall score.
About ACTA: Founded in 2002, Qingdao ACTA Biotechnology Co., Ltd. supplies MCC, colloidal MCC, CMC, HPMC, HEMC, and modified starch, so buyers can consolidate several cellulose ingredients in one order. See About ACTA and the facility and supply capability page for company details.
There is no universal cutoff. Confirm the supplier’s grade definition, test concentration, temperature, measurement method, and specified range before you compare products.
Sodium CMC is generally water-soluble, but dispersion and hydration depend on the grade and preparation conditions.
Add it gradually into a well-circulated liquid, ensure good dispersion, allow hydration time, and check for interfering ingredients.
No. Run application-specific trials against a control and set the dosage from measured performance.
Many applications exist, but verify grade suitability, documentation, and regulatory requirements for your intended use and market.
Sometimes, but only after controlled testing of dosage, hydration, compatibility, and finished-product performance.
Grade, specification, quantity, packaging, delivery terms, freight, payment terms, and quotation validity all matter. Compare quotations on equivalent technical and commercial terms.
Compare viscosity under equivalent test conditions, including concentration, temperature, measurement method, and sample preparation. Then review DS, moisture, other critical specifications, and performance in your intended formulation. Similar viscosity values alone do not prove that two grades are interchangeable.
Before you buy, request the current TDS, a representative or batch-specific COA, and the SDS. Depending on the application and destination market, you may also need food-grade or pharmaceutical compliance documents, relevant certificates, and supporting test reports, so confirm that each document applies to the selected grade and intended use. On arrival, check product identity, batch number, COA match, package condition, and quantity.
Choosing the right low viscosity CMC is about more than meeting a viscosity specification. The right grade should also suit your formulation, processing conditions, and target performance.
At Qingdao ACTA Biotechnology Co., Ltd., we help customers evaluate cellulose-based ingredients for different industrial and formulation requirements.
Contact our team to discuss your low viscosity CMC requirements, including:
To help us respond more accurately, please share your intended application, target viscosity and test conditions, estimated order quantity, and destination country.
Ready to discuss your project? Contact ACTA Biotechnology for product information and a quotation for low viscosity CMC.
We look forward to discussing your requirements and helping you identify a suitable solution for your application.
Richard Wang
International Sales & Technical Content
Qingdao ACTA Biotechnology Co., Ltd.
Website: https://www.actabiotechnology.com/
Contact ACTA | View the CMC product page
Richard Wang, International Sales & Technical Content, Qingdao ACTA Biotechnology Co., Ltd.
Email: wangpengfei@actabiotechnology.com | Phone: +86-532-85693212 | WhatsApp: +86-18263653583
Please confirm product availability, specifications, and commercial terms for your specific requirements before placing an order.
