By ACTA Biotechnology Technical Team | September 22, 2026 | Beverage Stabilizers in MCC in oat milk
MCC in oat milk is increasingly evaluated as part of a broader stabilization strategy for plant-based beverages. In particular, when manufacturers need to improve particle suspension, reduce sedimentation, and maintain a consistent mouthfeel during storage, MCC can become an important component to evaluate. At the same time, however, oat milk is a complex multi-phase system containing oat solids, proteins, lipids, minerals, and water.
Therefore, stability problems rarely come from a single factor. Instead, sedimentation, creaming, viscosity changes, and poor redispersion can result from the interaction of several formulation and processing variables.For this reason, colloidal MCC is often evaluated together with other functional ingredients rather than as a standalone solution. For example, CMC, modified starch, xanthan, emulsifiers, or other stabilizing components may be incorporated depending on the specific stability problem. However, the effectiveness of an MCC-based system depends on how well the selected grade, dosage, dispersion, hydration, and processing conditions are matched to the formulation. Consequently, successful oat milk stabilization requires not only choosing the right ingredient, but also understanding how that ingredient functions within the complete beverage system.
MCC is a commonly evaluated stabilizing ingredient for oat-based beverages, particularly where manufacturers want suspension support without excessively increasing beverage viscosity. Colloidal MCC can contribute to suspension stability by helping create a structured system around suspended particles, and it can also support body — but it rarely works alone. In most commercial formulations it operates alongside CMC, modified starch, xanthan gum, or emulsifiers, each contributing a distinct function. Understanding the complete system matters as much as understanding MCC itself.
Scope: This guide focuses on the physical stability and formulation aspects of using MCC in oat milk. It does not replace product-specific regulatory, microbiological, nutritional, or shelf-life validation. Food-additive status and permitted use levels for cellulose-based ingredients vary by market. Manufacturers should confirm current requirements against sources such as the FDA’s food additive status list or EFSA’s food additives database for their target markets, alongside their own quality and regulatory teams.
MCC in oat milk can help improve suspension stability, reduce sedimentation, and support a more consistent beverage structure. Colloidal MCC is typically evaluated together with other stabilizers such as CMC, depending on the oat base, protein, oil, minerals, processing conditions, and target sensory profile. There is no universal dosage; the appropriate grade and concentration should be confirmed through formulation-specific testing.
About ACTA Biotechnology: ACTA Biotechnology supplies cellulose-based ingredients — including microcrystalline cellulose, colloidal MCC, CMC, HPMC, and HEMC — for food, pharmaceutical, and industrial applications. For plant-based beverage applications, ACTA can support grade screening, sample evaluation, technical documentation, and commercial supply discussions.
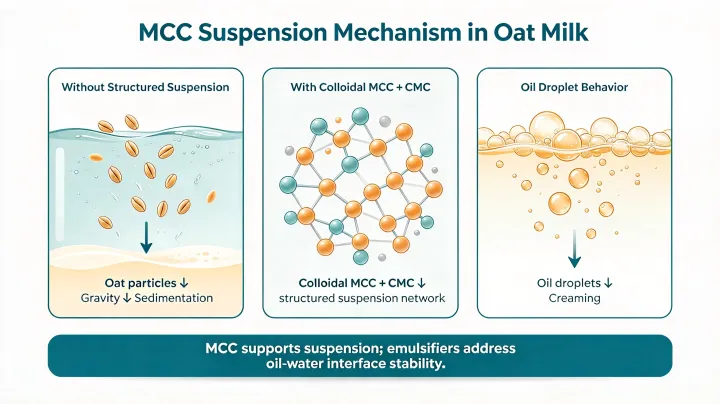
Title:MCC Suspension Mechanism in Oat Milk Caption:How colloidal MCC supports suspended particles in oat milk while emulsion stability requires separate control
Microcrystalline cellulose (MCC) is an insoluble cellulose material that, formulated as colloidal MCC, can build a fine particulate network throughout an aqueous system. This network physically supports suspended particles rather than simply thickening the surrounding liquid. As a result, colloidal MCC can help oat milk hold insoluble oat solids in suspension without pushing the beverage toward an unpleasantly thick or syrupy texture.
This distinction matters because many formulators instinctively reach for a thickener whenever a beverage shows sedimentation. Raising viscosity and improving suspension are not the same task. A formulation can become noticeably thicker while particles continue to settle, because bulk viscosity and structural suspension work through different mechanisms. Higher viscosity does not automatically mean better suspension. This is the single most important idea in this guide — later sections simply point back to it where it applies, rather than re-explaining it each time.
Conventional MCC and colloidal MCC should not automatically be treated as interchangeable materials. Ordinary microcrystalline cellulose is primarily an insoluble particulate ingredient. Colloidal MCC, by contrast, is engineered specifically for aqueous beverage systems, and many colloidal MCC grades are formulated with CMC to provide complementary suspension and rheology functions. The first supplier-qualification question a formulator should ask is simple: is this product ordinary MCC or colloidal MCC, and does it already contain another functional hydrocolloid? Where the product is intended for cross-border sale, this is also the point to check current additive status against a resource such as the Codex Alimentarius food additive provisions for the target markets.
MCC should not be treated as a universal fix, either. It can contribute to suspension and body, but it is not an emulsifier — Section 3.4 covers why that distinction matters. The actual outcome in any given formulation depends on grade, concentration, particle characteristics, CMC content, shear history, homogenization, protein, oil, mineral salts, and pH, so results should always be confirmed through the manufacturer’s own testing.
Oat milk is a multi-phase system: insoluble oat particles, dissolved and dispersed protein, vegetable oil, minerals, and sometimes added starch or sweeteners, all suspended in water. A beverage that appears uniform on Day 0 can still separate, sediment, or thicken over the following weeks — a full testing schedule for catching this is set out in Section 9.
Several factors make oat milk particularly demanding to formulate:
Choosing an oat milk stabilizer is rarely a matter of picking whichever ingredient has the highest viscosity or the lowest price. Different stabilizers solve different problems.
| Ingredient | Primary Functional Role | Typical Formulation Focus |
|---|---|---|
| Colloidal MCC | Suspension structure, particle stabilization, moderate body | Sedimentation and suspended solids |
| CMC | Aqueous-phase rheology, water binding, hydration support | Viscosity and suspension support |
| Xanthan gum | Strong rheological modification at low concentrations | Suspension and flow behavior |
| Modified starch | Body, texture, viscosity | Mouthfeel and formulation structure |
| Emulsifier | Oil-water interfacial stabilization | Creaming and emulsion quality |
| Gellan gum | Low-level network structuring in suitable systems | Suspension and network formation |
| Carrageenan | Structure and interaction with specific components | Texture and protein-related stabilization |
| Pectin | Rheology and stabilization in suitable systems | Texture and colloidal stability, mainly at lower pH |
| Main Problem | First Ingredient/System to Evaluate | Why |
|---|---|---|
| Bottom sediment | Colloidal MCC | Suspension structure |
| Weak aqueous rheology | CMC | Water-phase viscosity |
| Strong creaming | Emulsifier + homogenization | Oil-water interface |
| Very thin body | Modified starch | Body and texture |
| Heavy particle load | MCC + CMC / MCC + xanthan | Suspension + rheology |
| Gritty texture | Process + particle control | Dispersion/agglomeration |
| Post-UHT instability | Heat/process + stabilizer system | Thermal interaction |
| Mineral-related instability | Review complete stabilizer system | Mineral–hydrocolloid interaction |
MCC and CMC are both cellulose-based but not interchangeable. Colloidal MCC contributes structural suspension; CMC primarily supports water-phase viscosity and hydration. Increasing CMC alone can raise viscosity without improving suspension (see Section 1). Sedimentation problems are usually screened against colloidal MCC systems first, while weak aqueous rheology points more toward CMC.
Xanthan gum can provide strong rheological modification at relatively low use levels, but at higher concentrations it can produce a gummy mouthfeel. MCC-based systems use a different suspension mechanism and may give a different sensory profile, though the actual outcome always depends on grade, dosage, and the rest of the formulation — controlled trials remain essential. Where particle load is genuinely heavy, an MCC + xanthan combination is worth evaluating.
Modified starch contributes body and creaminess rather than suspension, so the two are frequently used together: MCC to hold particles in suspension, starch to build body. Relying on starch alone to fix sedimentation raises viscosity without solving the underlying issue.
This is one of the most important distinctions in oat milk formulation: MCC is not an emulsifier. An emulsifier manages the oil-water interface — droplet formation, interfacial stability, coalescence. These are functions MCC cannot replace. A manufacturer can face two genuinely different problems at once: bottom sediment and a top cream layer. More MCC may help the first while doing little for the second.
Gellan gum builds stability through a different mechanism than MCC, shows different texture and flow behavior, and is sensitive to minerals. MCC tends to be preferable when the target is suspension support plus body rather than a gel-like network.
Carrageenan’s performance depends strongly on type, concentration, ions, protein, pH, and thermal history. Compare it against MCC on sedimentation, viscosity, mouthfeel, and thermal stability rather than assuming equivalence.
Pectin is more established in acidic beverage systems. For neutral oat milk, evaluate a given grade directly. MCC is often the more relevant product type to evaluate first when particle suspension, not pectin-specific functionality, is the goal.
There is no single best stabilizer for every oat milk. A light oat beverage with low oil and mild sedimentation may need only a simple MCC/CMC system. A creamy, higher-oil oat milk may need an emulsifier, homogenization, a suspension stabilizer, and a texture modifier together. The correct system is determined by the product specification, not by the ingredient name alone.
| Ingredient | Suspension | Rheology | Body | Emulsion |
|---|---|---|---|---|
| MCC | ●●● | ●● | ●● | — |
| CMC | ●● | ●●● | ●● | — |
| Xanthan | ●●● | ●●● | ● | — |
| Modified Starch | ● | ●● | ●●● | — |
| Emulsifier | — | — | — | ●●● |
Title:MCC vs CMC vs Xanthan in Oat Milk Caption:Functional comparison of common stabilizer components used in oat milk formulation.
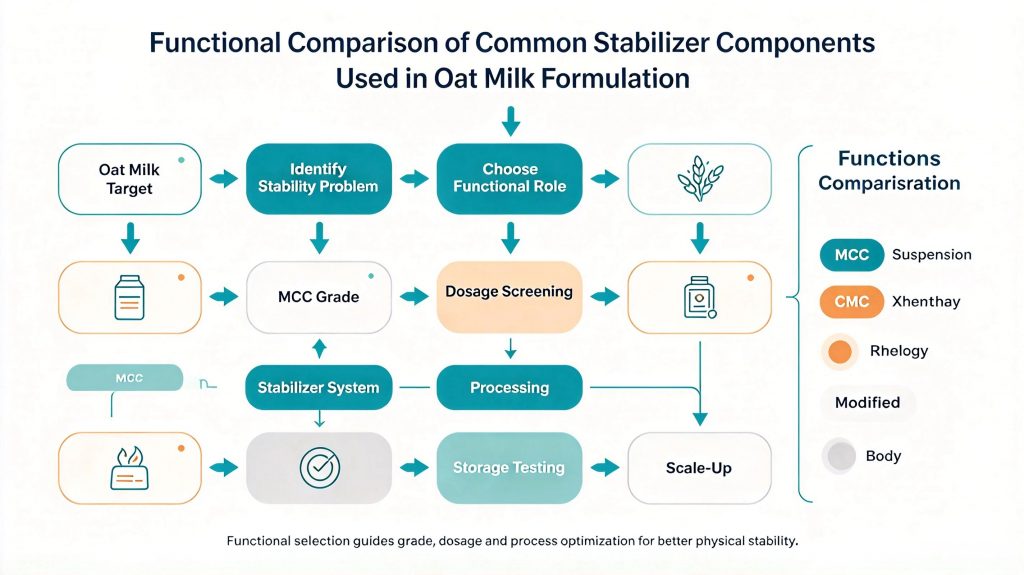
Title:Oat Milk Stabilizer Formulation Workflow Caption:A step-by-step formulation workflow for diagnosing instability and screening MCC-based stabilizer systems.
Many oat milk formulations need more than one functional mechanism at once. Because these functions are genuinely different, a combination system with clearly assigned roles usually outperforms a single ingredient pushed to a high dosage. Where a formulation also targets other plant-based beverage stabilizer systems, the same role-based logic applies across the product line.
| Ingredient | Primary Formulation Role |
|---|---|
| Colloidal MCC | Suspension structure, particle stabilization, body |
| CMC | Aqueous-phase rheology and water management |
| Modified starch | Body, texture, structural support |
| Xanthan gum | Strong rheological modification and suspension support |
| Emulsifier | Oil-water interface stabilization |
| Combination | Functional Logic | What to Watch For |
|---|---|---|
| MCC + CMC | Suspension structure + aqueous-phase support | No universal ratio — validate for each formulation |
| MCC + Modified Starch | Suspension + body/texture | Starch is heat- and shear-sensitive — test under the real process |
| MCC + Xanthan | Suspension + stronger rheology | Total viscosity can rise faster than expected |
| MCC + CMC + Modified Starch | Suspension + aqueous rheology + body | More variables to control — add only if each provides a measurable benefit |
| MCC + CMC + Xanthan | Suspension + rheology + strong flow control | High risk of over-thickening if all three rise together |
A formulation can gradually accumulate ingredients until the system becomes expensive and hard to troubleshoot. For every ingredient, ask: what specific function does this provide? What happens if it’s removed or reduced?
The goal is the smallest practical combination that reliably meets the stability, sensory, and processing requirements — not the lowest concentration of every ingredient, and not the highest number of stabilizers either. Every additional ingredient should be justified by a side-by-side trial.
| Trial | MCC | CMC | Modified Starch | Xanthan | Main Purpose |
|---|---|---|---|---|---|
| A | Low | Low | — | — | Basic suspension screening |
| B | Medium | Low | — | — | Stronger MCC contribution |
| C | Low | Medium | — | — | CMC comparison |
| D | Medium | Medium | — | — | MCC + CMC optimization |
| E | Medium | Medium | Low | — | Body + suspension |
| F | Medium | Medium | — | Low | Suspension + stronger rheology |
Exact percentages should come from your own trials. This matrix compares functional relationships; it is not a predetermined commercial formula.
There is no universal MCC dosage for oat milk. A more reliable sequence is grade screening, then dosage screening, then process validation. Different viscosity grades of the same ingredient can perform quite differently even at an identical MCC dosage.
| MCC Concentration | Approx. Quantity per 1,000 kg Batch |
|---|---|
| 0.10% | 1 kg |
| 0.20% | 2 kg |
| 0.30% | 3 kg |
| 0.40% | 4 kg |
| 0.50% | 5 kg |
These figures are examples for experimental design, not universal commercial recommendations. In practice, formulators often start with a screening range like this and identify the lowest concentration that meets stability, sensory, and processing requirements with a sufficient safety margin.
| MCC Level | Stability | Viscosity | Sensory | Relative Cost |
|---|---|---|---|---|
| Low | Poor | Low | Light | Low |
| Medium-low | Improved | Moderate | Acceptable | Moderate |
| Medium | Strong | Moderate | Acceptable | Moderate |
| Medium-high | Strong | Higher | May become heavy | Higher |
| High | Strong | High | May become undesirable | Highest |
The more useful question isn’t “does more MCC work better,” but what additional stability benefit each incremental unit delivers. Once diminishing returns appear, further increases mainly add cost (see Section 10 for the full cost-in-use logic).
| Formulation Situation | Grade Direction to Screen | Main Evaluation |
|---|---|---|
| Light oat milk | Lower-structure grade | Suspension + mouthfeel |
| High insoluble solids | Stronger suspension grade | Sedimentation + redispersion |
| High viscosity already | Lower viscosity grade | Stability at acceptable viscosity |
| MCC + CMC system | Colloidal grade with defined CMC contribution | Total rheology |
| UHT oat milk | Heat-process compatible grade | Pre/post-UHT stability |
Illustrative screening logic, not a universal grade recommendation.
Grade selection should account for whether the product is conventional MCC or colloidal MCC. A supplier should clearly identify product type, whether CMC is already included, recommended application range, and the conditions under which viscosity was measured. If a formulation only reaches required stability at an unacceptably high viscosity, the more productive next step is usually testing a different grade rather than raising the current dosage.
Even a well-chosen MCC grade at an appropriate dosage can’t deliver consistent results if the process around it is inconsistent. Processing is as much a part of the formulation as the recipe itself.
6.1 Dispersion and hydration are not the same event. A powder can appear evenly distributed while still requiring more time to fully hydrate. If added faster than it can disperse, local over-concentration can cause agglomeration. This can lead to uneven viscosity that has nothing to do with total MCC dosage. Dry premixing and liquid premixing can both improve wetting, depending on equipment and formulation.
6.2 Homogenization should support the formulation, not compensate for poor dispersion. If MCC hasn’t been properly hydrated beforehand, aggressive homogenization can mask the problem temporarily. The inconsistency often reappears during storage.
6.3 Heat treatment can change everything that came before it. Evaluate formulations both before and after the intended thermal process. A useful pilot procedure compares a pre-heat, immediate post-heat, cooled, and stored sample.
6.4 Cooling and shear history are process variables too. Two formulations with identical ingredients can develop different structures if their shear or cooling histories differ. Recording the complete process history, not just the recipe, is essential when troubleshooting or transferring a formulation between sites.
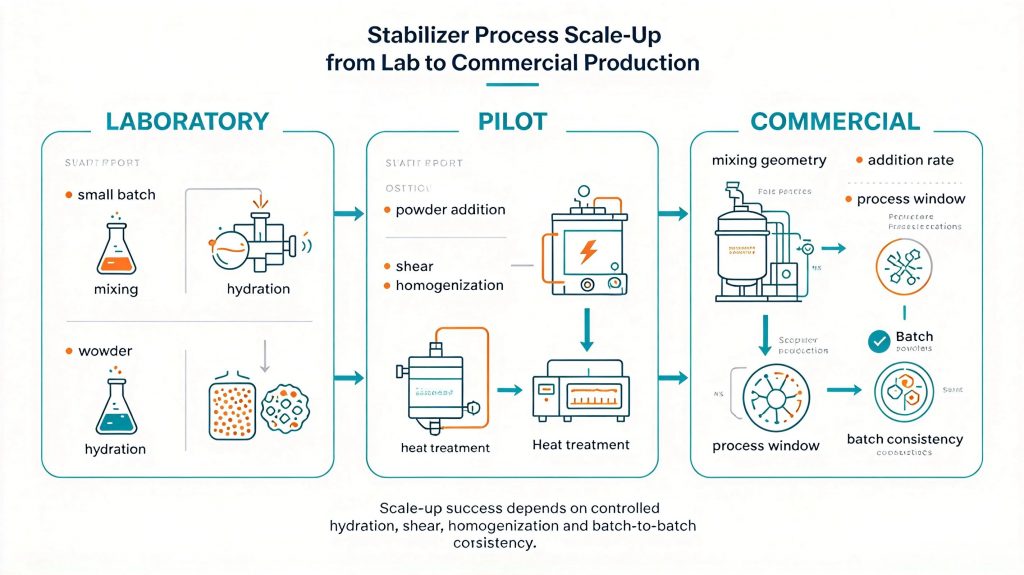
Title:Oat Milk Lab to Commercial Scale-Up Caption: Key process variables that can change when an MCC-based oat milk formulation moves from laboratory to pilot and commercial production.
A formulation that performs well on the lab bench doesn’t automatically perform the same way at pilot or commercial scale. Production equipment introduces different mixing geometry, powder addition rates, shear history, and heat-treatment profiles than a small laboratory batch does.
7.1 Four main scale-up variables: powder distribution consistency, MCC hydration time/conditions, commercial homogenization comparability, and whether the production heating profile reproduces the desired stability. Evaluate these together, since they interact.
7.2 Powder addition rate becomes more critical at scale. If the addition rate exceeds the system’s ability to disperse it, agglomerates form. The final product can then show inconsistent viscosity even at the correct total dosage.
7.3 Mixing time is not the same as hydration time. A common scale-up mistake is reducing hydration time to move faster. A visually uniform mixture isn’t necessarily a fully developed stabilizer system.
7.4 Do not change formulation and process simultaneously. Keep the formulation constant while optimizing the process, then keep the process constant while optimizing the formulation, then validate the combined system.
7.5 Establish a process window, not one exact number. It’s more useful to set an acceptable operating range than to rely on one fixed value.
7.6 Batch-to-batch consistency is the real commercial test. When a new MCC lot behaves differently, compare it directly against the previous lot and investigate the COA before changing the commercial formulation.
Supplier Qualification Tip: If a supplier recommends a dosage without asking about your oat solids, oil content, mineral system, and processing conditions, treat that recommendation as a starting point rather than a finished formulation.
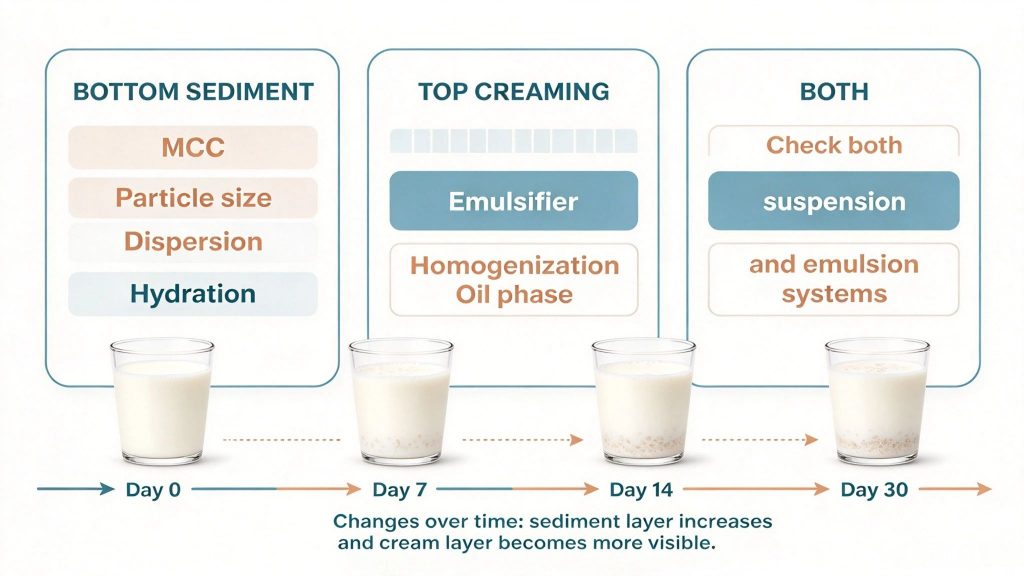
Title:Oat Milk Stability Troubleshooting Caption:A troubleshooting framework for separating sedimentation, creaming, and combined instability in oat milk
When an oat milk formulation shows instability, the instinctive response is often to increase stabilizer dosage. That’s rarely the most efficient fix, because different failure modes point to different root causes.
bottom separation; top separation; uniform thickening with poor stability; gritty texture; or good Day-0 stability with poor long-term stability.
Potential causes include large oat particles, insufficient MCC, poor hydration, poor dispersion, inadequate processing, or long storage time. Sedimentation despite an already-adequate MCC level often points to a process gap rather than a formulation gap.
Fine, loose sediment redisperses easily; dense, compact sediment resists returning to suspension. Evaluate both how much sediment forms and how easily it redisperses.
A standardized redispersion test — inverting or shaking a defined number of times and recording time, inversions, and uniformity — turns redispersion into an objective, comparable measurement.
Creaming is primarily an emulsion problem (see Section 3.4). Investigate oil concentration, emulsifier choice, and homogenization before increasing MCC dosage.
Troubleshoot the oil phase and the suspension-stabilizer side separately, rather than raising one hydrocolloid to solve both.
Excessive viscosity often results from the total stabilizer system rather than MCC alone. Therefore, instead of reducing a single component immediately, rebalance the complete stabilizer system and reassess its overall contribution to viscosity. On the other hand, when the beverage has a thin body, the appropriate adjustment depends on the underlying problem: if sedimentation is also occurring, MCC may be worth evaluating for suspension support; whereas, if the beverage is simply too thin sensorially, modified starch may be more appropriate for building body. In either case, the formulation should be adjusted according to the specific performance target rather than by changing one ingredient in isolation.See the companion guide on protein drink stabilization for how body-building decisions shift at higher protein load.
Can stem from large particles, agglomerated stabilizer, incomplete dispersion, or poor homogenization — check these before changing dosage.
If stable before heating but unstable after, investigate the thermal process first, not the MCC dosage.
| Observation | Possible Causes | First Things to Check | Potential Direction |
|---|---|---|---|
| Bottom sediment | Large particles, weak suspension | MCC, particle size, dispersion | Optimize MCC system |
| Compact sediment | Aggregation, poor redispersion | Particle structure, storage | Improve suspension/process |
| Top cream layer | Oil instability | Emulsifier, homogenization | Optimize emulsion system |
| Top + bottom separation | Multiple mechanisms | Oil and solids separately | Optimize both phases |
| Thin body | Low solids/rheology | Total solids, CMC, starch | Adjust body-building system |
| Excessive viscosity | Too much hydrocolloid | CMC, xanthan, starch, MCC | Rebalance total system |
| Gritty texture | Agglomeration/particles | Dispersion, homogenization | Correct process first |
| Stable Day 0 only | Long-term instability | Day 7/14/30 evaluation | Improve storage stability |
| Instability after heating | Thermal interaction | Pre/post-heat comparison | Adjust process/system |
| Poor redispersion | Compact sediment | Particle aggregation | Optimize MCC/process |
| Batch-to-batch variation | Raw material/process variation | Mixing and ingredient lots | Tighten process controls |
| Trial | MCC | CMC | Sediment Day 7 | Day 14 | Day 30 | Viscosity | Sensory |
|---|---|---|---|---|---|---|---|
| A | Low | Low | High | High | High | Low | Light |
| B | Medium | Low | Low | Medium | Medium | Moderate | Good |
| C | Medium | Medium | Low | Low | Low | Moderate | Good |
| D | High | Medium | Very low | Very low | Low | High | Heavy |
8.12 A simple troubleshooting workflow: identify exactly what’s happening → isolate the mechanism → change one major variable → validate by repeating the standardized test across Day 0/7/14/30.
8.13 When the problem is not the stabilizer. Large particles may need upstream particle-size control. Poor emulsification may need a different emulsifier. Protein aggregation may need pH, mineral, or thermal adjustment. Poor dispersion may need a better addition process. In all of these cases, adding more MCC only increases cost.
Day-0 appearance isn’t the finish line for stability testing (see Section 2). Tracking trends over time, not a single snapshot, is what actually validates a commercial formulation.
9.1 A structured testing schedule evaluates sedimentation, redispersion, creaming, viscosity, appearance, and sensory characteristics at Day 0, 7, 14, 30, and extended storage, aligned to the product’s intended shelf life.
9.2 Score sedimentation and redispersion consistently using a numeric scale rather than yes/no, applied consistently across grades, dosages, suppliers, and processes.
9.3 Document every trial — formulation, process, results, and a brief conclusion — to prevent re-testing the same unsuccessful formulation without realizing it. The same discipline applies to food hydrocolloid selection generally, not just MCC trials.
9.4 Illustrative Oat Milk MCC Screening Protocol
| Parameter | Screening Design |
|---|---|
| MCC grades | 2–3 candidate grades |
| MCC level | 0.10%, 0.20%, 0.30%, 0.40%, 0.50% |
| Control | Current formulation without MCC |
| Mixing | Keep mixing conditions constant |
| Homogenization | Keep pressure/conditions constant |
| Day 0 | Appearance, viscosity, sedimentation |
| Day 7 | Sedimentation, creaming, redispersion |
| Day 14 | Stability and sensory |
| Day 30 | Extended stability |
| Measurements | Viscosity, visual stability, sediment height, redispersion |
The concentrations above are illustrative screening levels, not a universal dosage recommendation. Actual use levels should be established through formulation-specific testing.
The most common purchasing mistake is comparing suppliers by price per kilogram alone.
10.1 Price per kg vs. cost per ton of beverage.
| Grade | Price | Trial Dosage | Ingredient Cost per 1,000 kg Beverage |
|---|---|---|---|
| Grade A | $2.80/kg | 0.40% | $11.20 |
| Grade B | $3.40/kg | 0.25% | $8.50 |
Grade B costs more per kilogram but less per 1,000 kg of finished beverage at these illustrative dosages.
10.2 Calculate the total stabilizer-system cost.
| Component | System A | System B |
|---|---|---|
| MCC | 0.30% | 0.20% |
| CMC | 0.10% | 0.20% |
| Modified starch | 0.20% | 0.30% |
| Total stabilizer load | 0.60% | 0.70% |
System B uses less MCC but more of the other ingredients. The relevant figure is total stabilizer cost, not any single ingredient viewed in isolation.
10.3 Diagnose before reducing dosage. Cost optimization should follow, not precede, an understanding of the failure mechanism.
10.4 Look for the minimum effective level — with an adequate safety margin against normal production variation. Pushing too close to the stability threshold can turn a minor lot or temperature variation into visible sedimentation.
10.5 Improve processing before increasing dosage. If poor dispersion means only part of the added MCC is functioning effectively, improving addition and hydration can deliver the same stability at lower cost.
10.6 Evaluate the whole cost picture — formulation cost, processing cost, quality risk, and supply risk together.
Cost-in-Use Tip: The most expensive MCC is not necessarily the one with the highest price per kilogram. It may be the material that creates inconsistent production and forces the plant to compensate with additional stabilizers.
A successful laboratory sample is the beginning of supplier qualification, not the end of it.
11.1 Confirm exactly what is being purchased. “MCC” can mean conventional MCC, colloidal MCC, or an MCC/CMC system. A supplier should clearly identify product name, grade, type, composition, physical form, viscosity characteristics, moisture spec, packaging, storage conditions, shelf life, and lot ID system, along with additive-status confirmation for the buyer’s target market.
11.2 Review the TDS, then verify with the COA. A TDS describes the product generally; a COA describes an individual lot. This is where batch-to-batch consistency becomes visible. A viscosity number is only meaningful when test concentration, temperature, equipment, and hydration procedure are understood.
11.3 Test more than one production lot before final approval. A single sample demonstrates compatibility, not long-term consistency. A practical approach: one sample for laboratory screening, then two or three for repeatability, then additional lots for commercial verification.
11.4 Compare suppliers under identical conditions — same oat base, oil, protein, minerals, dosage, mixing, hydration, homogenization, heat treatment, packaging, and evaluation schedule.
11.5 Establish change-control expectations up front — which manufacturing-site, raw-material-source, or specification changes require notification, sample re-evaluation, or full requalification.
11.6 Evaluate supply reliability alongside technical performance — MOQ, lead time, capacity, packaging, export documentation, and forecast coordination.
11.7 A three-level approval process.
| Level | Focus | Typical Requirements |
|---|---|---|
| Level 1 — Laboratory | Basic performance | Acceptable dispersion, hydration, viscosity, suspension, sensory |
| Level 2 — Pilot | Process robustness | Powder handling, mixing, hydration, homogenization, heat treatment |
| Level 3 — Commercial | Long-term reliability | Multi-batch consistency, documentation, supply reliability, change control, cost-in-use |
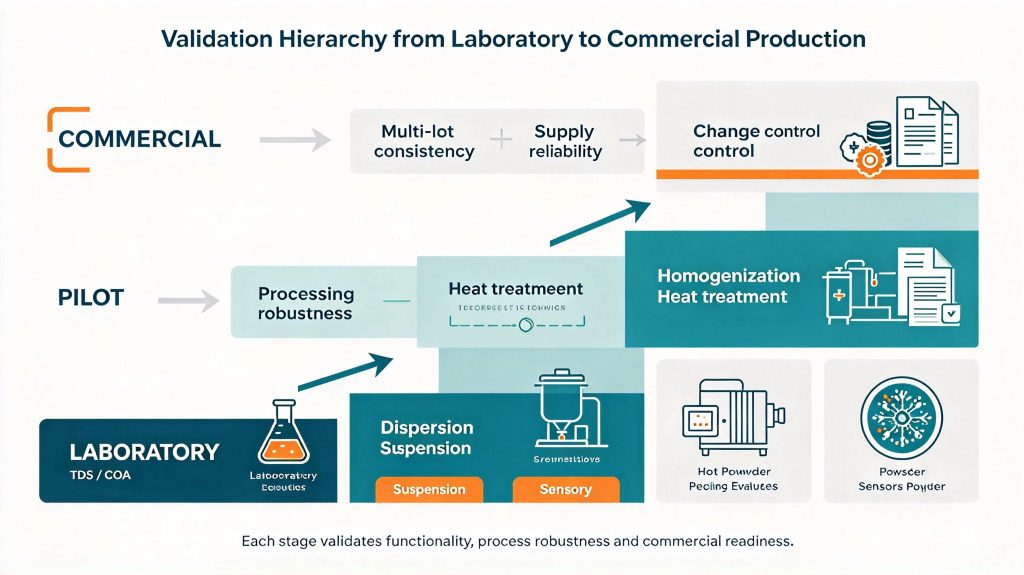
Title:MCC Supplier Qualification Process Caption:A three-level framework for qualifying MCC performance, consistency, documentation, and commercial supply capability.
12.1 Start with the application, not a generic price request.
| Buyer Information | Why It Matters |
|---|---|
| Oat solids | Determines suspended particle load |
| Protein | Affects thermal and colloidal behavior |
| Oil | Determines emulsion requirements |
| pH | Influences protein/hydrocolloid interactions |
| Minerals | Can affect hydrocolloid and protein behavior |
| Heat treatment | Changes final stability |
| Existing stabilizer system | Prevents unnecessary ingredient stacking |
| Main stability failure | Helps identify the correct mechanism |
12.2 Describe the failure, not just the ingredient name — bottom sediment, top creaming, phase separation, poor redispersion, or post-heat instability, and when it occurs.
12.3 Record sample identity precisely — supplier, product name, grade, lot number, dates, TDS/COA references, storage conditions, and quantity.
12.4 Keep a trial report for every formulation — unique trial number, exact MCC identity, complete matrix, precise concentration, and addition method. This turns development into a defensible, reproducible record.
When requesting an MCC or colloidal MCC evaluation, provide:
When requesting an MCC or colloidal MCC evaluation, send the following details to ACTA. In this way, a well-specified inquiry allows the supplier to propose relevant candidate grades from the first response, rather than requiring several rounds of back-and-forth before a meaningful recommendation can be made. As a result, providing sufficient formulation and process information at the beginning can make the evaluation more efficient and help narrow down suitable grades more quickly.
One-page development logic: Product target → Matrix (oat solids, protein, oil, minerals, pH) → Failure diagnosis → MCC grade → Dosage → Stabilizer system → Processing → Scale-up → Stability testing → Cost-in-use → Supplier.
Commercial approval checklist:
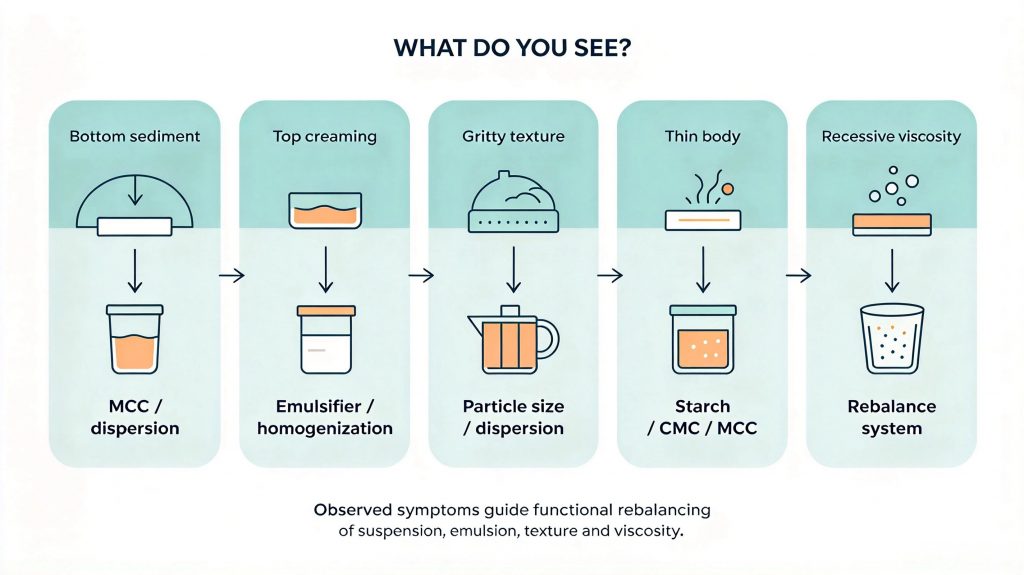
Title:Oat Beverage Stabilizer Decision Matrix Caption:Decision matrix for identifying the first formulation or process variable to evaluate when oat milk shows common stability problems.
Colloidal MCC can help build a particulate suspension network that supports insoluble oat particles and other suspended solids, contributing to physical stability and moderate body without relying primarily on bulk viscosity.
No. MCC primarily contributes suspension structure while CMC primarily supports aqueous-phase viscosity and hydration. They’re often used together rather than as substitutes (see Section 3.1).
There is no universal dosage — it depends on the grade, oat solids, protein, oil content, and the rest of the stabilizer system, and should be established through controlled screening (Section 5).
It can help reduce sedimentation when grade, dosage, dispersion, and hydration are all appropriate. However, if persistent sedimentation remains despite adequate MCC, the underlying problem may be related to processing, particle characteristics, or the overall stabilizer system rather than simply requiring a higher dosage (Section 8.2). Therefore, increasing MCC concentration should not automatically be the first response.
For beverage suspension applications, colloidal MCC is generally the more relevant product type to evaluate first because it is formulated for aqueous systems and many grades already include CMC (Section 1). However, the most suitable product still depends on the specific formulation, processing conditions, and target performance. Therefore, standard MCC and colloidal MCC should be evaluated according to their intended function rather than assumed to be interchangeable.
Not reliably — the two contribute different functions, and most formulations benefit from having both.
No — see Section 3.4 and Section 8.5 for why creaming and sedimentation need to be diagnosed and treated separately.
Instability often develops gradually — see Section 9 for a structured testing schedule.
Through a structured screening protocol across multiple grades and dosage levels, with sedimentation, redispersion, viscosity, and sensory evaluation at Day 0, 7, 14, and 30 (Section 9.4).
Confirm exactly what’s being purchased, review TDS and lot-specific COAs, test more than one lot, compare suppliers under identical conditions, and evaluate cost-in-use rather than price per kilogram (Section 11).
The right approach to MCC in oat milk starts with the beverage, rather than the ingredient itself. First, define what the finished product needs to achieve and, then, identify the actual instability mechanism before selecting and screening candidate grades and dosages. Next, build the simplest stabilizer system that meets the target, while also standardizing dispersion and hydration. After that, validate the formulation through storage testing and scale-up to ensure that laboratory performance can be translated into practical production conditions.
In addition, calculate the true cost-in-use rather than comparing ingredient prices alone. At the same time, qualify the supplier through documentation, multiple-lot evaluation, and demonstrated consistency. Ultimately, MCC can be an effective suspension solution for oat milk; however, its value comes from being used with a clear functional purpose alongside CMC, modified starch, xanthan gum, or emulsifiers. In other words, MCC should be selected and evaluated as part of a defined stabilization strategy, rather than being treated as a universal fix.
Send your current formulation, main stability problem, processing conditions, target dosage range, and expected volume (see the Inquiry Template in Section 12). ACTA can provide candidate colloidal MCC grades, TDS, COA, samples, and commercial information for your internal evaluation.
The final grade and dosage should always be confirmed through your own laboratory, pilot, and commercial validation.
Manufacturers should verify current regulatory status and cite primary sources directly for compliance purposes; the resources above are starting points, not a substitute for consulting official databases.
